
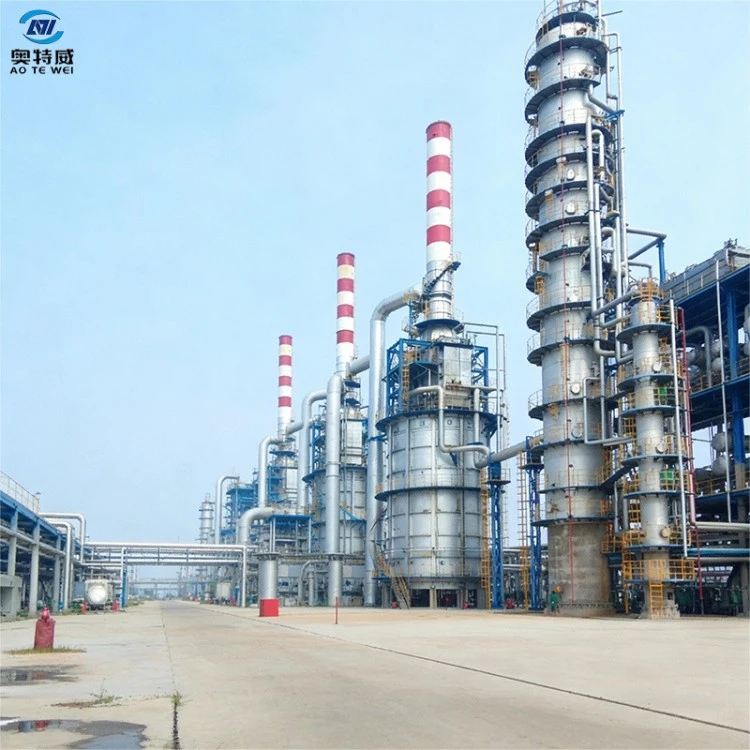

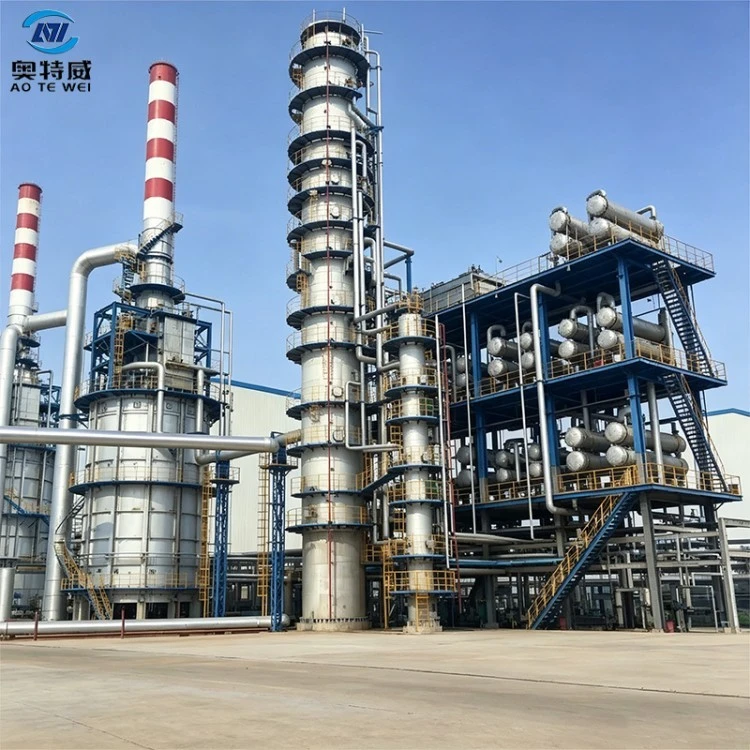
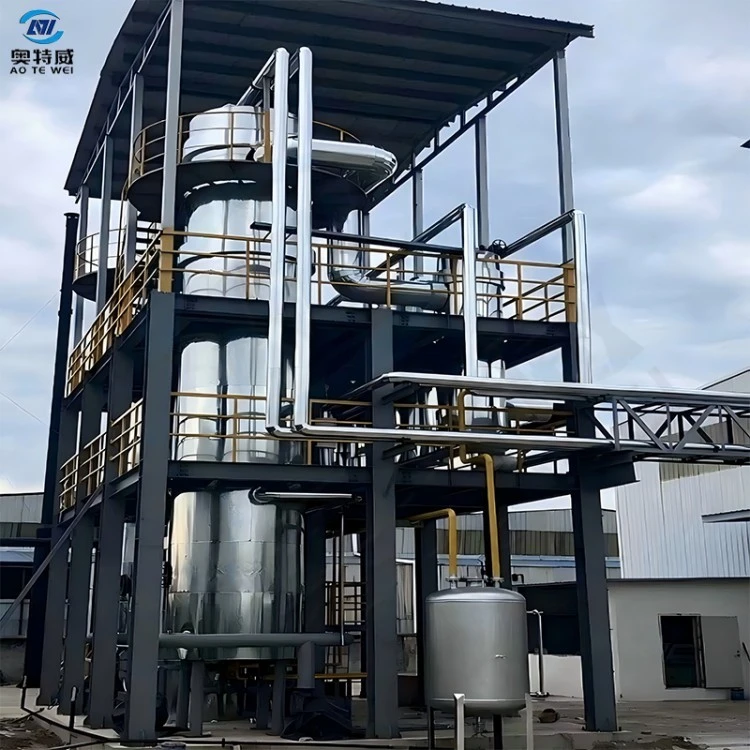
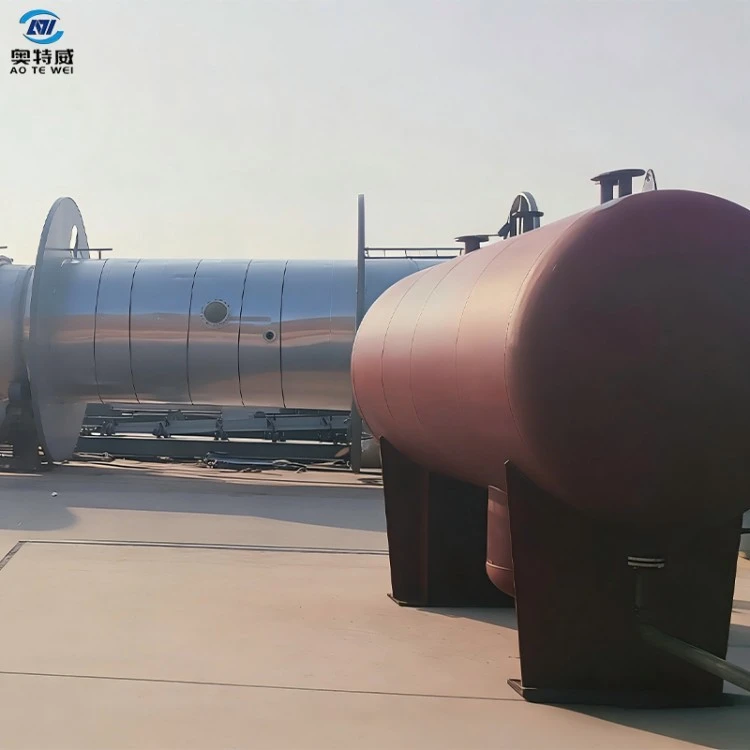
Shangqiu Aotewei Environmental Protection Equipment Co., Ltd. is one of the leading manufacturers and suppliers of industrial distillation plant in China. We are committed to providing high quality customized products with competitive price. If you're going to buy ISO certified industrial distillation plant, welcome to get quotation from our factory.
Product Name
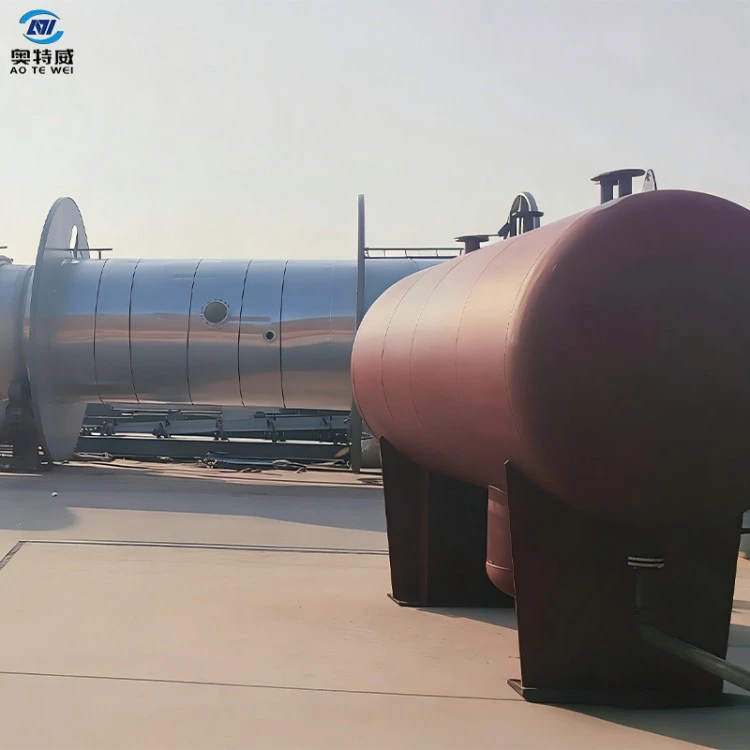
General-purpose Complete Industrial Distillation Plant. It is a modular industrial equipment developed for distillation and purification requirements across multiple industries and diverse feedstocks. With combinable distillation, rectification, condensation and pre-treatment units, it supports multiple process modes including atmospheric-pressure, negative-pressure, continuous and batch operation. It realizes precise separation and purification of hundreds of materials such as crude oil, chemical solvents, waste mineral oil, vegetable oil and pharmaceutical intermediates, and delivers stable and reliable industrial distillation solutions for petroleum, chemical, environmental-protection, pharmaceutical and food industries. Reference investment: Starting from USD 350,000.
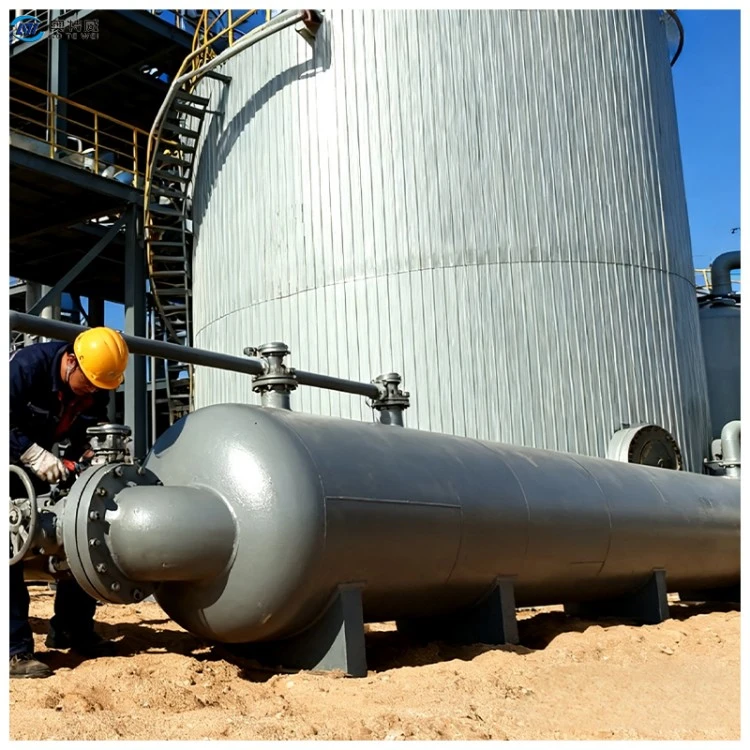
| Technical Parameter of the Pyrolysis plant | |||
| 1 | Suitable Raw Materials | Waste Engine Oil, Fuel Oil, Crude Oil | Waste Engine Oil, Fuel Oil, Crude Oil |
| 2 | Structure | Horizontal Rotation Type | Horizontal Rotation Type |
| 3 | Reactor Size | φ2600×6600mm φ2800×8000mm φ3000×8800mm |
φ1500×2000mm φ1800×4000mm φ2000×600mm |
| 4 | Work Pressure | Normal Pressure | Normal Pressure |
| 5 | Oil Yield | 85%~95% | 85%~95% |
| 6 | Work Pressure | Normal Pressure | Normal Pressure |
| 7 | Power | 15-25kw/H | 15-25kw/H |
| 8 | Heating Method | Indirect Heating | Indirect Heating |
| 9 | Type of Installation | Without Foundation | Without Foundation |
| 10 | Cooling Method | Cycling Water | Cycling Water |
| 11 | Noise dB (A) | ≤ 85 | ≤ 85 |
| 12 | Cooling Method | Cycling Water | Cycling Water |
| 13 | End Product | Non-standard Diesel Oil | Non-standard Diesel Oil |
| 14 | Manpower | 4-6/shift | 2-4/shift |
Features
High-vacuum low-temperature rectification system:
Adopting modular combination of standard process sections, the Industrial Distillation Plant can flexibly match pre-treatment, distillation, condensation, rectification and post-processing units according to distillation requirements of different materials. One single set of equipment covers distillation and purification demands of multiple industries. It adapts to processing scenarios for different feedstocks without replacing core main equipment.
Stable-operation system for wide working conditions:
The core distillation unit of the Industrial Distillation Plant covers a broad pressure range from high vacuum of -0.095 MPa to atmospheric pressure, as well as a wide temperature span from low to high temperature. It handles various hard-to-process materials featuring high boiling point, high viscosity, thermal sensitivity and easy crystallization. Boasting strong adaptability to working-condition fluctuations, it achieves stable non-stop 7×24-hour operation.
Precise component separation control:
Equipped with high-precision temperature, pressure and flow sensing units together with an adjustable reflux-ratio control system, it realizes accurate cutting and separation of components with different boiling points. The maximum single-stage distillation purity can reach over 99 %, meeting purification accuracy requirements from various industries.
Fully-closed safe and eco-friendly structure:
The whole system of the Industrial Distillation Plant runs in fully-closed mode without leakage of volatile materials. A three-stage tail-gas treatment unit is configured to purify organic waste gas and odors. Meanwhile, an automatic residue discharge system reduces manual material contact. It generates no secondary pollution and complies with environmental-protection emission requirements of most countries worldwide.
Advantage
Flexible investment and high customizability:
Equipment units can be flexibly configured according to customers' throughput, feedstock properties, site conditions and budget. We supply both standard complete-set equipment and undertake large-scale industrial non-standard customized projects. Investment thresholds cover full scenarios from lab-scale test, pilot test to large-scale industrial production.
High separation efficiency and low material loss:
Optimized column internals and flow-channel design, combined with precise reflux control, greatly boost separation efficiency and effectively reduce decomposition and loss of materials during distillation. The maximum material recovery rate can exceed 98 %, remarkably improving customers' raw-material utilization benefit and product added value.
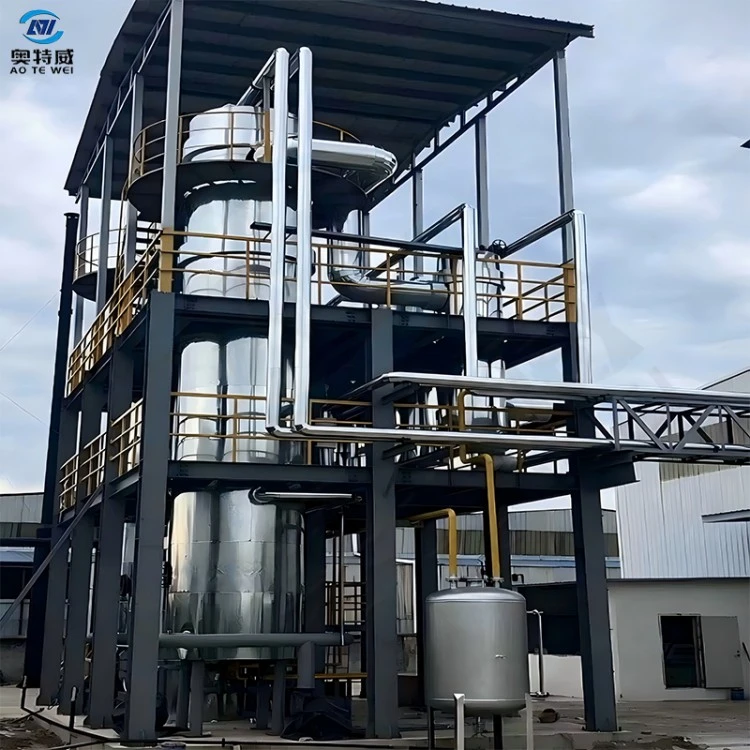
Optimized energy consumption and controllable operating costs:
Equipped with a waste-heat recovery system, it recovers waste heat from high-temperature distillates and kettle bottom residues for feed preheating, substantially cutting steam and power consumption. Compared with conventional distillation equipment, energy consumption per unit product decreases by 15-25 %, bringing outstanding long-term economic benefits.
Stable, durable and easy-to-maintain:
Core pressure vessels are manufactured strictly in accordance with national standards via automatic welding, ultrasonic non-destructive testing and hydrostatic test, with a designed service life of more than 15 years. Thanks to the modular design, each unit can be independently disassembled and inspected. Routine maintenance is simple and convenient, and downtime for maintenance is short without disrupting overall production progress.
Application Scenarios
- Environmental-protection & resource-recovery industry: Regeneration of waste mineral oil, refining of pyrolysis oil, recovery of chemical waste liquid, oil-sludge treatment and resource utilization of kitchen waste oil. It realizes reduction and resource-oriented treatment of hazardous waste, helping enterprises dispose of waste in compliance with regulations while generating extra profits.
- Bio-energy industry: Pre-treatment of biodiesel feedstock, crude glycerine purification, ethanol distillation and separation of bio-based chemicals. It meets full-process purification demands of the bio-energy industrial chain and helps bio-energy enterprises lower costs and raise efficiency.
- Mining and metallurgy industry: Recovery of mining extractants, treatment of metallurgical waste liquid, purification of rare- and-precious-metal solutions and tar processing. It enables recycling of chemical materials and cuts raw-material and hazardous-waste disposal costs for mining and metallurgy enterprises.
- Scientific research and pilot-test field: New-process R&D as well as lab-scale and pilot-scale experiments for universities and research institutes. Process parameters can be flexibly adjusted to acquire complete process data for industrial-scale production and provide reliable design basis for process scale-up.
Packing & Shipping
- Heavy-duty equipment including large columns, reaction kettles and storage tanks are bare-packed with anti-rust and anti-corrosion surface treatment. Key flange openings and instrument interfaces are sealed with dust-proof cover plates to prevent foreign-object ingress during transportation. Steel-structure frames, platforms and supports are packed in sections with clear marking and differentiation.
- Small precision components such as precision instruments, sensors, solenoid valves, control cabinets, valve-pipe fittings and column internals are individually packed in shock-proof and moisture-proof solid-wood cases filled with buffer protective materials. Each component is marked with clear serial number and name for easy on-site checking and installation.
- Complete technical documents are delivered together with goods: general assembly drawings of equipment, pipeline layout drawings, automatic-control-system logic manuals, operation & maintenance instructions, material certificates of equipment, pressure-vessel supervision-inspection reports, hydrostatic test reports, commissioning schemes, plus full-set documents required for import-export customs declaration and clearance.
- Clear labels of component serial number, name and material are attached to all equipment parts, together with detailed packing lists. It facilitates customers' rapid on-site checking, hoisting and positioning installation, lowering on-site installation difficulty and cycle.
FAQ
Q1: What kinds of materials can this industrial distillation plant process?
A: This plant is a general purpose industrial distillation unit. It adapts to hundreds of materials across petroleum, chemical, pharmaceutical, food, environmental protection and other industries, including crude oil, waste mineral oil, mixed chemical solvents, vegetable oil, pharmaceutical intermediates, essence and flavor, pyrolysis oil, waste liquid, etc. Matching process schemes and equipment configurations can be customized according to boiling point, viscosity and impurity characteristics of feedstocks.
Q2: Can the plant realize continuous production? Is throughput customizable?
A: Absolutely yes. The plant supports stable 24 hour continuous operation with daily throughput ranging from 0.5 tons to 100 tons. Equipment dimensions and process configurations can be custom designed according to customers' actual throughput requirements. Meanwhile, it is also compatible with batch mode production. One unit handles both continuous and batch operation modes.
Q4: Can the plant process high viscosity, coking prone and heat sensitive materials?
A: Absolutely yes. Equipped with a high vacuum system, the plant lowers the boiling point of materials to achieve low temperature distillation and avoid thermal decomposition of heat sensitive materials. For high viscosity and coking prone materials, anti sticking scraper structure and low speed rotation design can be configured to effectively prevent wall sticking and carbonization of materials, meeting distillation demands for various hard to process feedstocks.
Q5: Does equipment installation require complex foundation? How long is the installation cycle?
A: Standard skid mounted units do not require large complex foundations; only flat hardened ground is needed for installation. For large scale industrial units, foundation design drawings will be provided based on equipment weight. On the premise that customers' civil works and utilities are ready, the installation and commissioning cycle for regular size equipment lasts 30 60 working days. Our professional technicians can be dispatched to provide on site installation, commissioning and operation training services.
Company Profile & Production Capacity
Shangqiu Aotewei Environmental Protection Equipment Co., Ltd. is a professional equipment-manufacturing enterprise integrating R&D, design, production, installation & commissioning, sales and after-sales service of complete sets of distillation, rectification, pyrolysis and resource-utilization equipment. With more than ten-year-long dedication to industrial distillation and resource-treatment-equipment sector, it possesses full-chain engineering service capabilities.
The company holds complete pressure-vessel manufacturing qualifications and boasts full capabilities for process development and equipment manufacturing ranging from laboratory bench-scale test, pilot test to large-scale industrial equipment. We supply standard complete-set equipment and also provide non-standard customized one-stop distillation solutions according to customers' feedstock properties, production-capacity requirements and site conditions.
The enterprise has a professional team of over 70 members consisting of senior engineers, professional technicians and senior technicians. It owns standardized production workshops fully equipped with plate rolling, welding, heat treatment, non-destructive testing and machining facilities. All equipment undergoes strict quality inspection and trial-run to guarantee safe, stable and efficient operation upon delivery.
Our products are exported to more than 30 countries and regions worldwide, serving enterprises in petrochemical, environmental-protection resource-recovery, pharmaceutical, food and bio-energy industries. We have won wide recognition and trust from customers at home and abroad by virtue of stable equipment performance, professional process design and comprehensive after-sales service. Always customer-oriented, we provide high-efficiency, energy-saving, eco-friendly and compliant industrial distillation equipment together with full-chain technical services.
Hot Tags: industrial distillation plant, China industrial distillation plant manufacturers, suppliers, factory



