
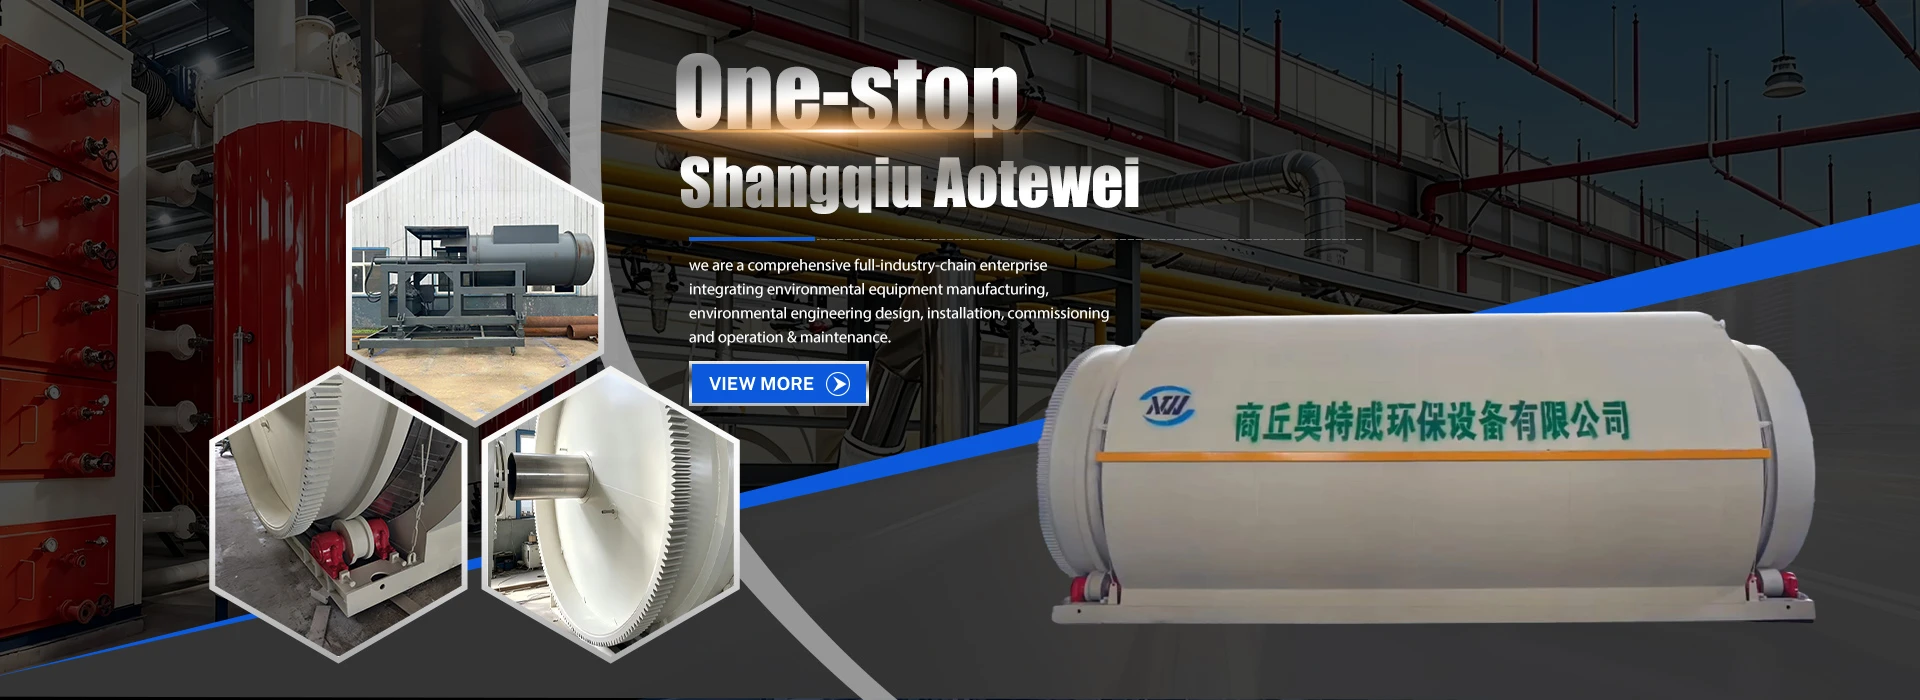
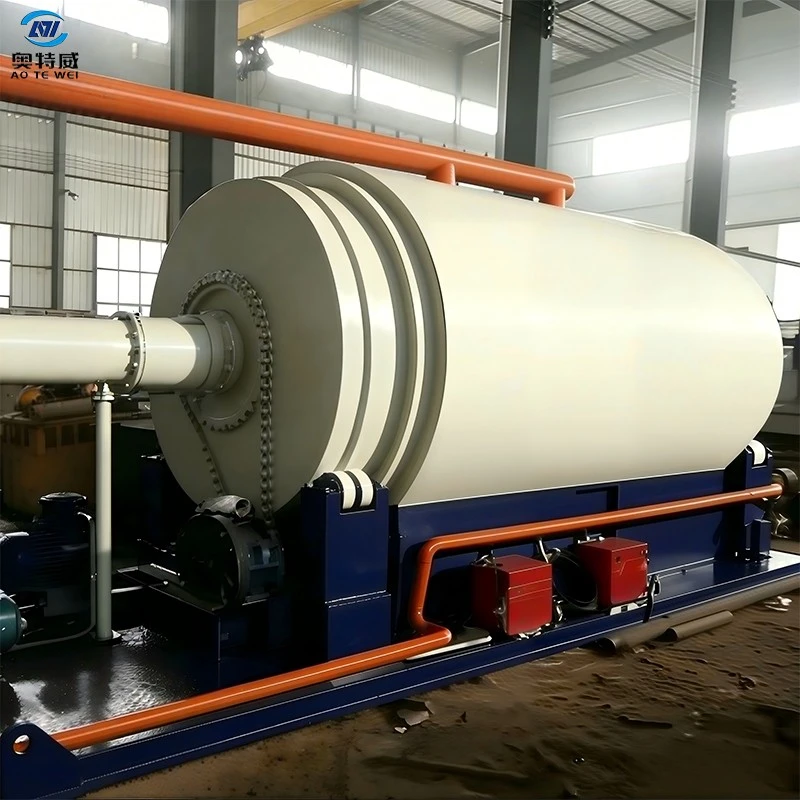
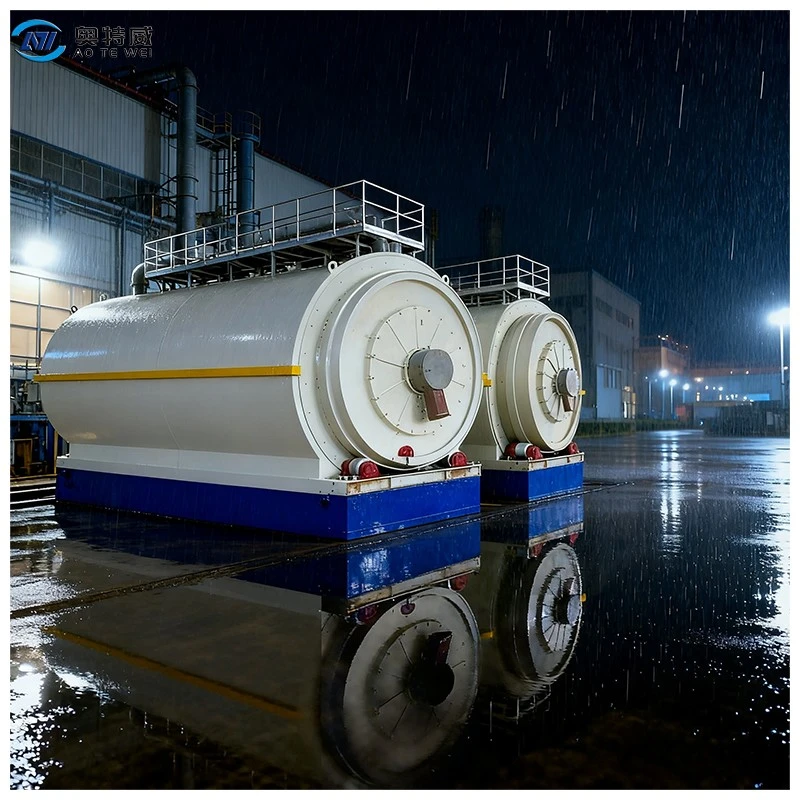
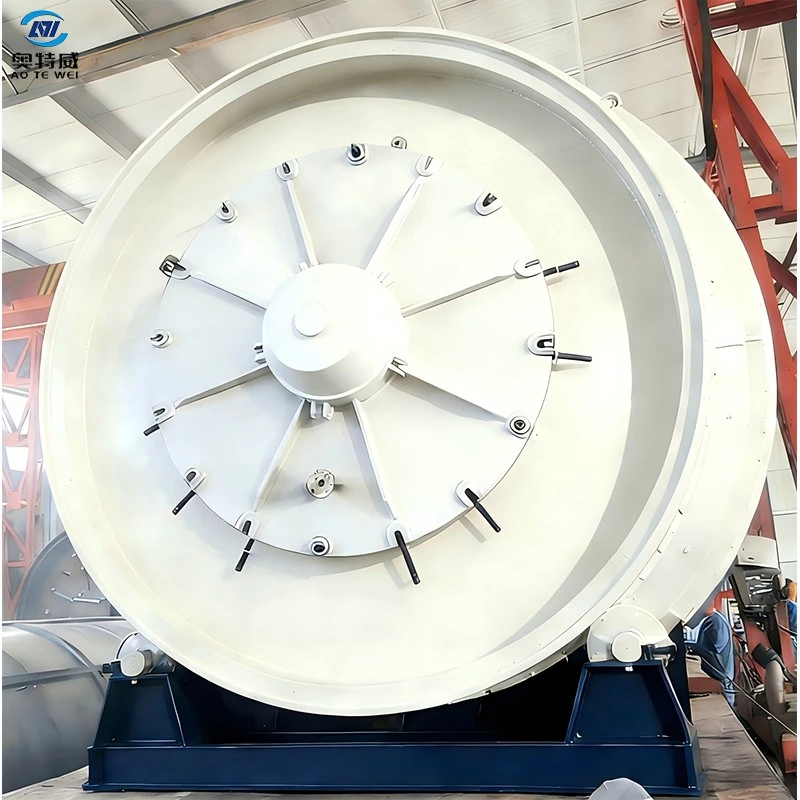
Shangqiu Aotewei Environmental Protection Equipment Co., Ltd. is one of the leading manufacturers and suppliers of oil shale pyrolysis plant in China. We are committed to providing high quality customized products with competitive price. If you're going to buy ISO certified oil shale pyrolysis plant, welcome to get quotation from our factory.
Products Description
Oil Shale Pyrolysis Plant
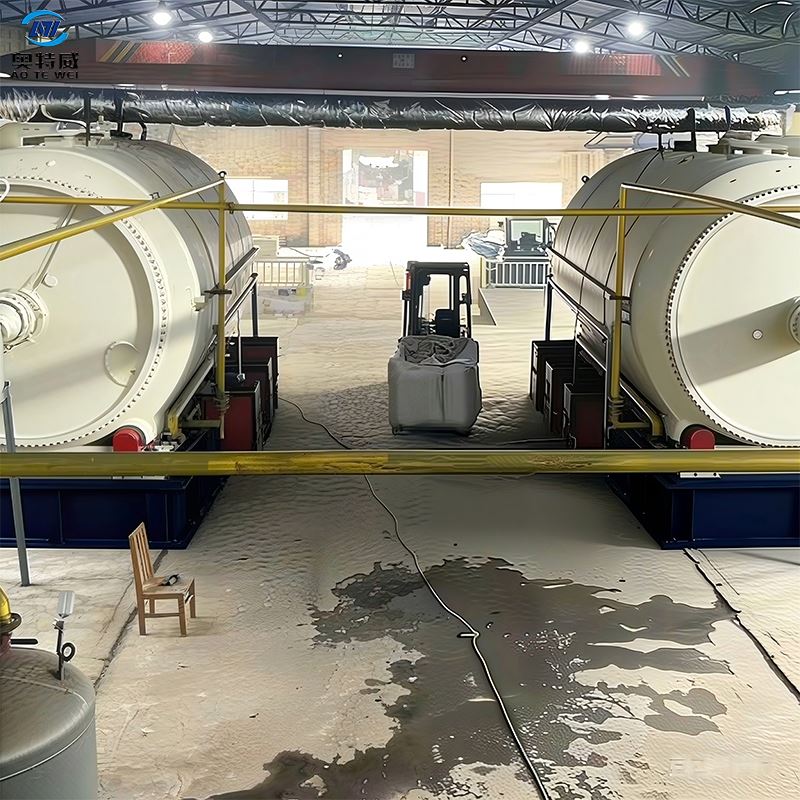
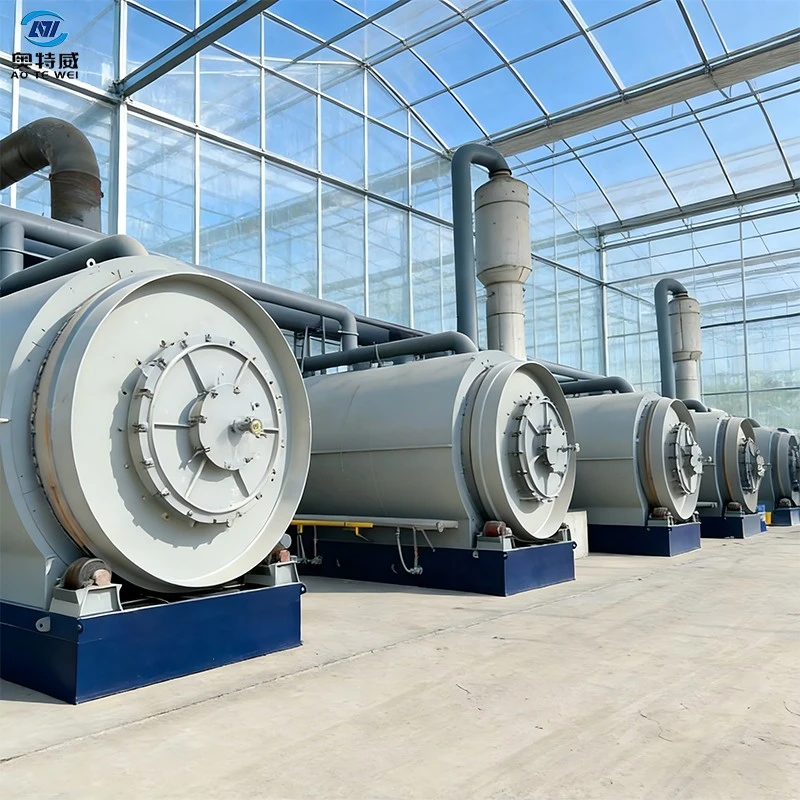
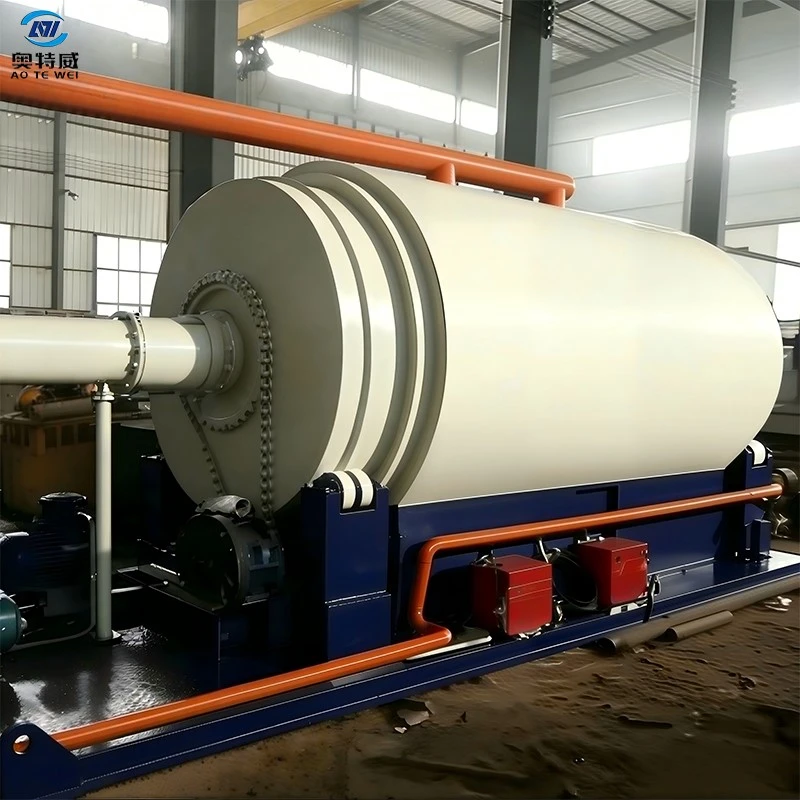
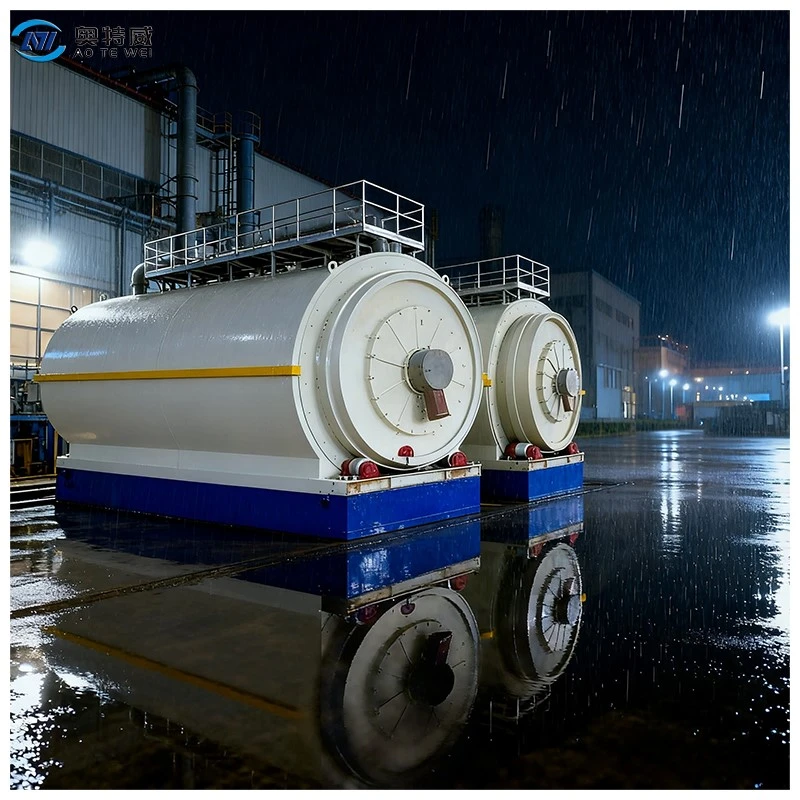
Oil Shale Pyrolysis Plant is special-purpose equipment developed for oil shale, the core raw material of unconventional oil and gas. Adopting sealed temperature-controlled high-temperature pyrolysis technology, it converts oil shale into high-value reusable products such as shale oil, semi-coke and combustible gas. Featuring modular skid-mounted construction, the plant delivers flexible processing capacity and low site-condition requirements. It is highly suitable for small-and-medium-sized oil shale mines and resource-utilization projects to realize on-site development and conversion of oil-shale resources.
Price Note: Actual equipment quotation is subject to raw-material market conditions, exchange rates and configurations. The reference price for 5-ton standard configuration is approximately USD 38,000 per set (excluding sea freight, taxes and on-site installation costs).
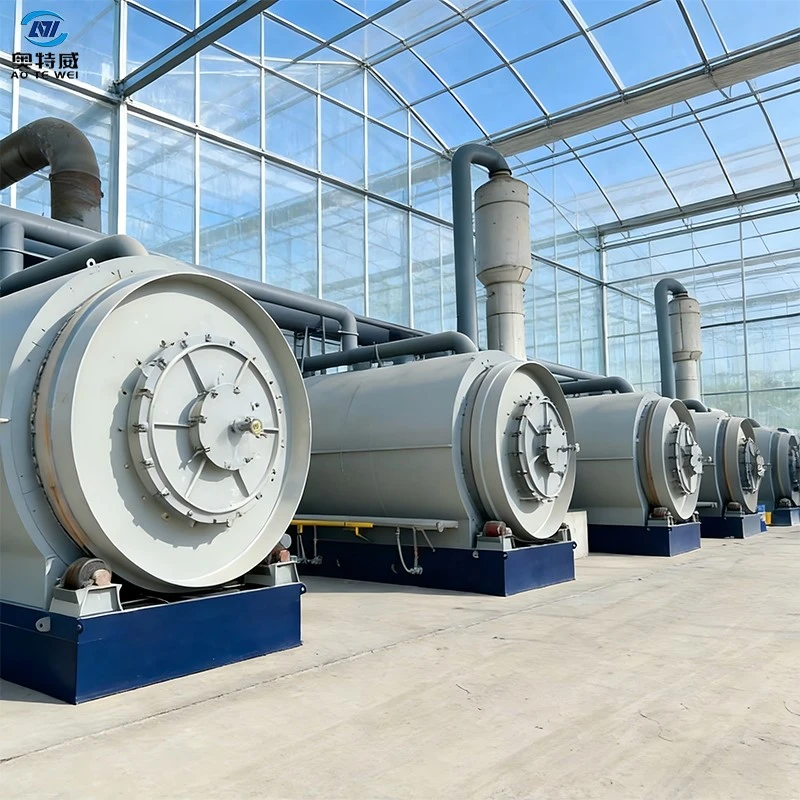
| Technical Parameter of the Pyrolysis plant | |||
| 1 | Suitable Raw Materials | Rubber/Plastic Products etc | Rubber/Plastic Products etc |
| 2 | Structure | Horizontal Rotation Type | Horizontal Rotation Type |
| 3 | Reactor Size | φ2600×6600mm φ2800×8000mm φ3000×8800mm |
φ1500×2000mm φ1800×4000mm φ2000×600mm |
| 4 | Capacity for One Batch | 8-10Mt; 12-15Mt; 18-20Mt | 1Mt; 3Mt; 5Mt |
| 5 | Oil Yield from Tyres | 40%~90% | 40%~90% |
| 6 | Work Pressure | Normal Pressure | Normal Pressure |
| 7 | Reactor Rotation Speed | 0.4R/M | 0.4R/M |
| 8 | Fuels Choice | Coal, Wood, Gas, Oil | Coal, Wood, Gas, Oil |
| 9 | Power | 15~22kw/h | 8~15kw/h |
| 10 | Cooling Method | Cycling Water | Cycling Water |
| 11 | Type of Drive | External Annular Gear | External Annular Gear |
| 12 | Heating Method | Direct Heating | Direct Heating |
| 13 | Type of Installation | Without Foundation | With Foundation / Integrated Base |
| 14 | Noise dB (A) | ≤ 85 | ≤ 85 |
| 15 | Operating Mode | Intermittent Operation | Intermittent Operation |
| 16 | Total Weight (MT) | 25~50 | 10~25 |
Features
① Special-purpose Temperature Control System for Oil Shale Pyrolysis
The main reactor is equipped with a high-precision temperature-control system. It can stably maintain the optimal pyrolysis temperature range of 450-550℃ according to oil content and material properties of oil shale, avoiding low oil yield caused by excessively high or insufficient temperature.
② Anti-coking Inner-wall Structural Design
Targeting the common coking issue during oil-shale pyrolysis, the reactor inner wall adopts a dedicated anti-coking structure to effectively reduce coke scale adhesion.
③ Co-processing Structure for Dust and Tail-gas Treatment
In view of the high-dust feature of flue gas from oil-shale pyrolysis, the unit is fitted with a multi-stage dust-removal system. It can efficiently remove particulate matters, sulfides and nitrogen oxides from flue gas, with emission indexes meeting environmental-protection requirements for mining areas.
④ Recycling System for Pyrolysis Combustible Gas
Non-condensable combustible gas generated from oil-shale pyrolysis is purified and delivered to the combustion chamber as heating fuel. It realizes self-sufficient production energy, greatly cuts consumption of external fuels such as coal and natural gas, and effectively reduces equipment operating costs.
Advantages
① High Shale-oil Recovery Rate
Pyrolysis process is optimized for the low-oil-content property of oil shale. The oil recovery rate for conventional oil-content oil shale can reach over 40%. It delivers better shale-oil output performance than ordinary general-purpose pyrolysis equipment and brings higher economic benefits for customers.
② Low Operating Energy Consumption
Relying on the recycling system of pyrolysis combustible gas, the equipment achieves over 90 % self-sufficiency of heating energy without massive consumption of external fuels.
③ Strong Environmental-protection Compliance
Complete sets of dust-removal, desulfurization and denitrification systems are integrated. Flue-gas emissions satisfy national and local environmental-protection standards for mining areas. The full-process closed-loop design prevents leakage of oil-gas and dust, enabling smooth passing of local mine environmental-protection acceptance.
④ Stable Long-term Operation with Low Maintenance Cost
Anti-coking structure and professional temperature-control system lower equipment failure rates. Core components adopt high-temperature-resistant and wear-resistant materials to adapt to harsh mining-site working conditions. It features long maintenance cycles and low later-stage operation-and-maintenance investment to guarantee stable long-term production.
Application Scenarios
Oil Shale Pyrolysis Plant applies to the following business scenarios:
Supporting Equipment for Small-and-medium-sized Oil-shale Mines: The equipment is deployed directly at mining sites to process mined oil shale on-site and produce shale oil, substantially cutting transportation costs of oil-shale raw materials and improving mine profits.
Small-scale Shale-oil Production Projects: Realize commercial resource utilization for low-grade oil-shale resources unsuitable for large-scale industrial development and create economic value for investors.
Energy Self-sufficiency Projects for Remote Mining Areas: Shale oil and combustible gas generated by the equipment supply fuel energy for mining sites, solving energy-supply difficulties in remote mines and lowering mine operating costs.
Disposal Projects for Oil-shale Tailings and Waste Rock: Cooperate with mines to treat tailings and waste rock produced from oil-shale mining, realize solid-waste reduction and resource utilization and satisfy mine environmental-protection control requirements.
Co-disposal of Oil Shale and Oil-bearing Sludge: The equipment supports mixed pyrolysis processing of oil shale and oil-bearing sludge, improves comprehensive resource-utilization rate and expands project business scope.
Packing & Shipping
Packing Method:
The main unit receives overall anti-rust and shock-proof protection; precision instruments, control valves and electric-control systems are packed in moisture-proof and shock-proof wooden cases; pipelines, fittings and wearing parts are bundled and packed by category, adapting to complex transportation conditions of mining areas.
Shipping Method:
Full-container sea freight is supported, as well as land trailer transportation for inland mining areas.
FAQ
Q1: Are there grade requirements for oil shale? Can low grade oil shale be processed?
A: This equipment fits various oil shale with oil content ranging from 6 % 15 %. Optimized for low grade oil shale, it can adjust pyrolysis temperature and material residence time to guarantee shale oil output. It can process oil shale feedstock with oil content as low as 5 %.
Q2: Can shale oil produced by oil shale pyrolysis be sold directly?
A: Produced shale oil can be directly sold as industrial fuel oil. It can also be further deep processed into finished oil products such as diesel and gasoline with supporting distillation equipment. Sales and application must comply with local oil product management and environmental protection regulations.
Q3: Will coking occur during equipment operation and how shall we handle it?
A: Dedicated anti coking inner wall structure plus precise temperature control system greatly reduce coking possibility. Conventional cleaning is carried out upon completion of normal production cycles to cut down maintenance hours.
Q4: What is the approximate payback period for investment in one set of equipment?
A: The payback period is affected by oil shale raw material cost, market selling price of shale oil and processing capacity.
Q5: Can equipment environmental protection emissions meet mining area requirements?
A: The equipment can be equipped with multi stage dust removal, desulfurization and denitrification systems. Flue gas emissions fully comply with national and local environmental protection standards for mining areas. There is no black smoke or peculiar odor; dust emission concentration is far below limit values, enabling smooth local environmental protection acceptance.
Production Process Flow
Raw-material Pretreatment: Crush, screen and dry mined oil shale. Control raw-material particle size ≤50 mm and raw-material moisture content within 10 % to improve pyrolysis efficiency.
Feeding & Sealing: Pretreated oil shale is fed into the pyrolysis reactor via closed feeding system. Close the feeding port to maintain oxygen-free conditions inside the reactor and prevent raw-material oxidation.
Precise Temperature-controlled Pyrolysis: The combustion chamber heats the reactor. Internal temperature is accurately maintained at 450-550℃. Oil shale undergoes pyrolysis under atmospheric and oxygen-free conditions to generate oil-gas mixture and semi-coke residues.
Multi-stage Oil-gas Separation: Oil-gas mixture enters the separation system to remove dust and heavy components inside oil gas; light-fraction oil-gas flows into the condensation system.
Condensation & Shale-oil Collection: Oil-gas enters the forced-circulation condensation system for fast heat-exchange and liquefaction. Liquid shale oil flows into the oil-storage tank to complete oil collection.
Combustible-gas Recycling: Treated non-condensable pyrolysis gas is sent into the combustion chamber as heating fuel for energy self-sufficiency.
Semi-coke Discharge & Treatment: Cool down the reactor after pyrolysis. Discharge semi-coke residues through closed slag-discharge system. Semi-coke can be used as fuel, building-material raw material or for further deep processing.
Tail-gas Purification & Discharge: Burned flue gas undergoes deep purification by desulfurization, denitrification and dust-removal processes, and is discharged via chimney after reaching emission standards to satisfy environmental-protection requirements.
Hot Tags: oil shale pyrolysis plant, China oil shale pyrolysis plant manufacturers, suppliers, factory


