

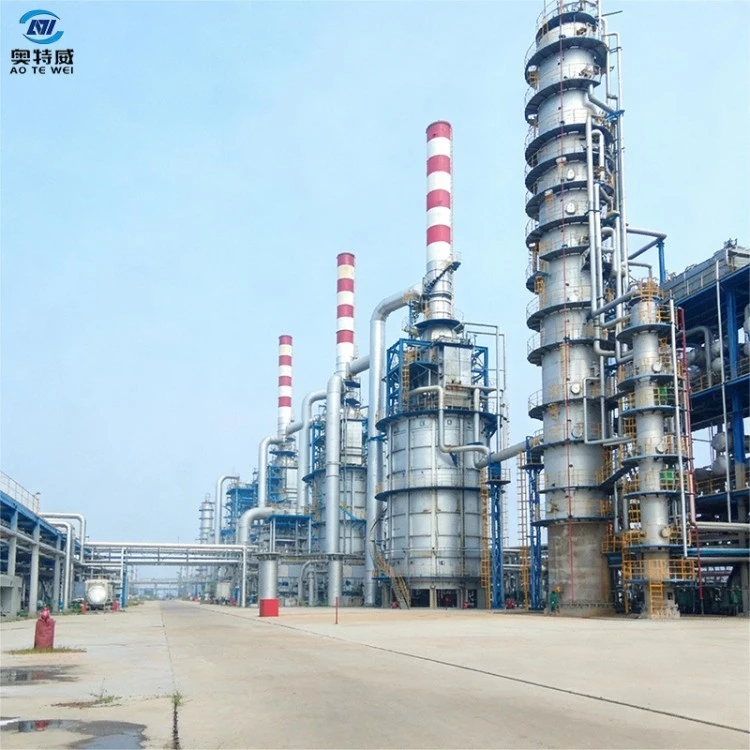
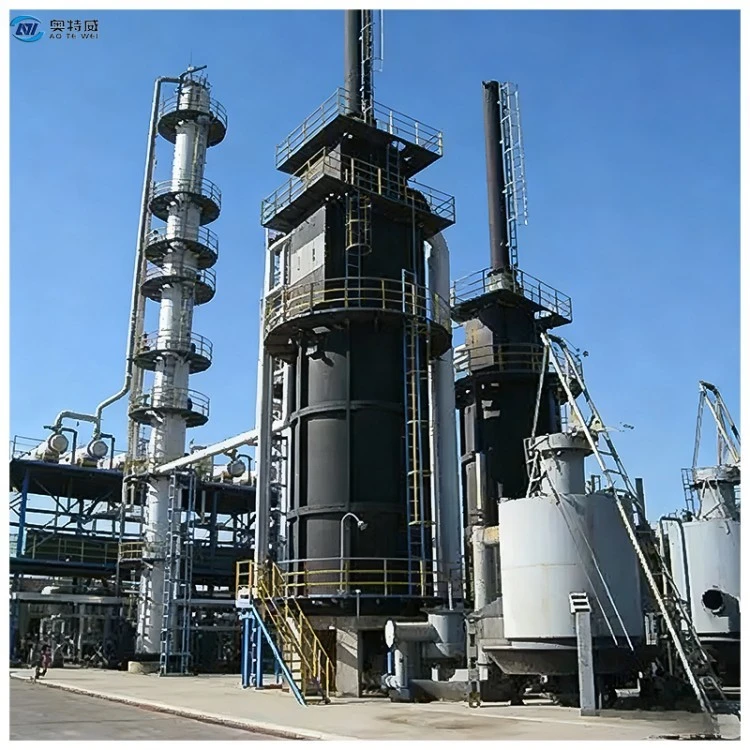

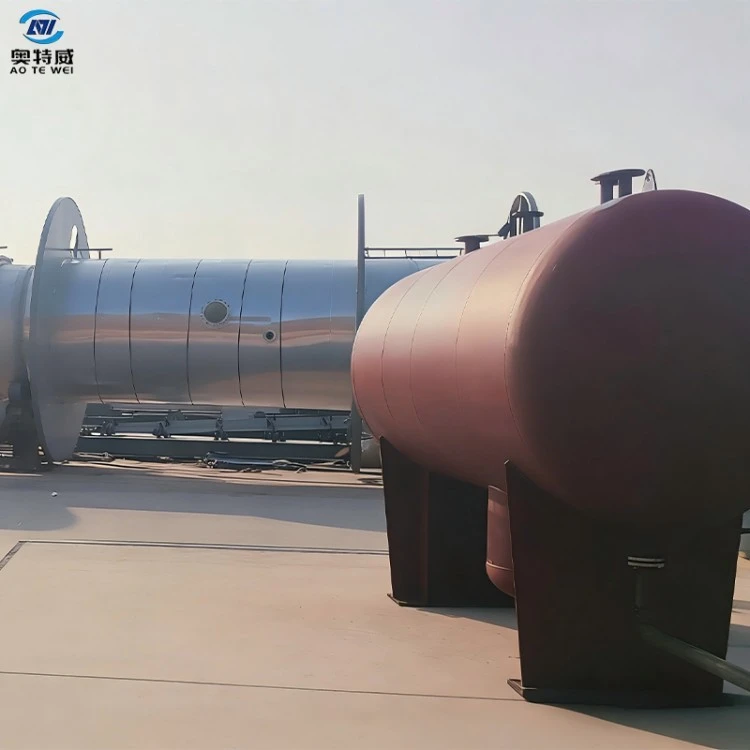
Shangqiu Aotewei Environmental Protection Equipment Co., Ltd. is one of the leading manufacturers and suppliers of chemical distillation plant in China. We are committed to providing high quality customized products with competitive price. If you're going to buy ISO certified chemical distillation plant, welcome to get quotation from our factory.
Product Name
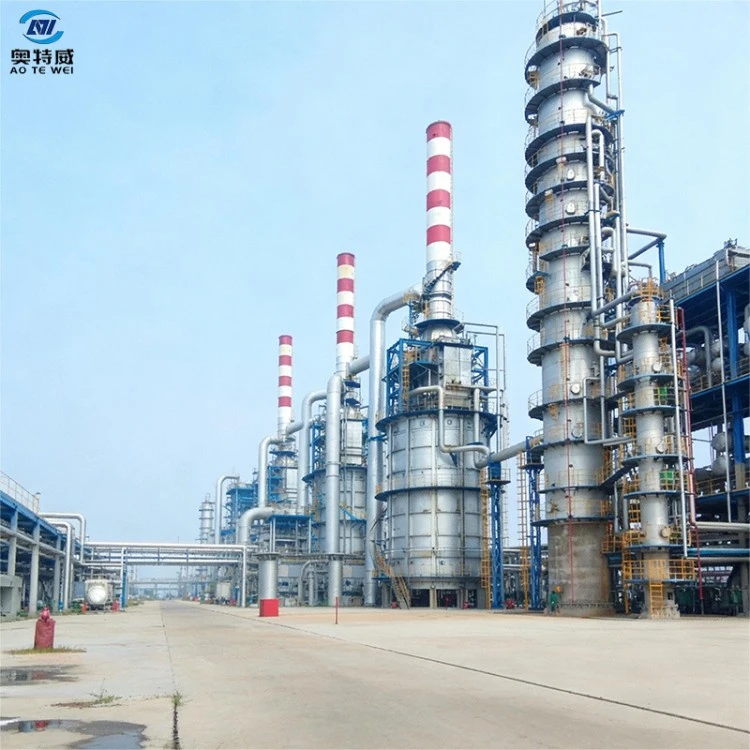
Chemical Distillation Plant Complete continuous distillation-separation equipment for chemical and petrochemical industries. It realizes component cutting and separation for various chemical waste liquids, mixed solvents and heavy-duty chemical raw materials to complete purification, recovery and resource-oriented treatment. It supports precise multi-component fractionation to produce qualified chemical feedstock. Reference Investment: 450,000 USD
| Technical Parameter of the Pyrolysis plant | |||
| 1 | Suitable Raw Materials | Waste Engine Oil, Fuel Oil, Crude Oil | Waste Engine Oil, Fuel Oil, Crude Oil |
| 2 | Structure | Horizontal Rotation Type | Horizontal Rotation Type |
| 3 | Reactor Size | φ2600×6600mm φ2800×8000mm φ3000×8800mm |
φ1500×2000mm φ1800×4000mm φ2000×600mm |
| 4 | Work Pressure | Normal Pressure | Normal Pressure |
| 5 | Oil Yield | 85%~95% | 85%~95% |
| 6 | Work Pressure | Normal Pressure | Normal Pressure |
| 7 | Power | 15-25kw/H | 15-25kw/H |
| 8 | Heating Method | Indirect Heating | Indirect Heating |
| 9 | Type of Installation | Without Foundation | Without Foundation |
| 10 | Cooling Method | Cycling Water | Cycling Water |
| 11 | Noise dB (A) | ≤ 85 | ≤ 85 |
| 12 | Cooling Method | Cycling Water | Cycling Water |
| 13 | End Product | Non-standard Diesel Oil | Non-standard Diesel Oil |
| 14 | Manpower | 4-6/shift | 2-4/shift |
Features
Multi-column Continuous Fractionation Process Configuration:
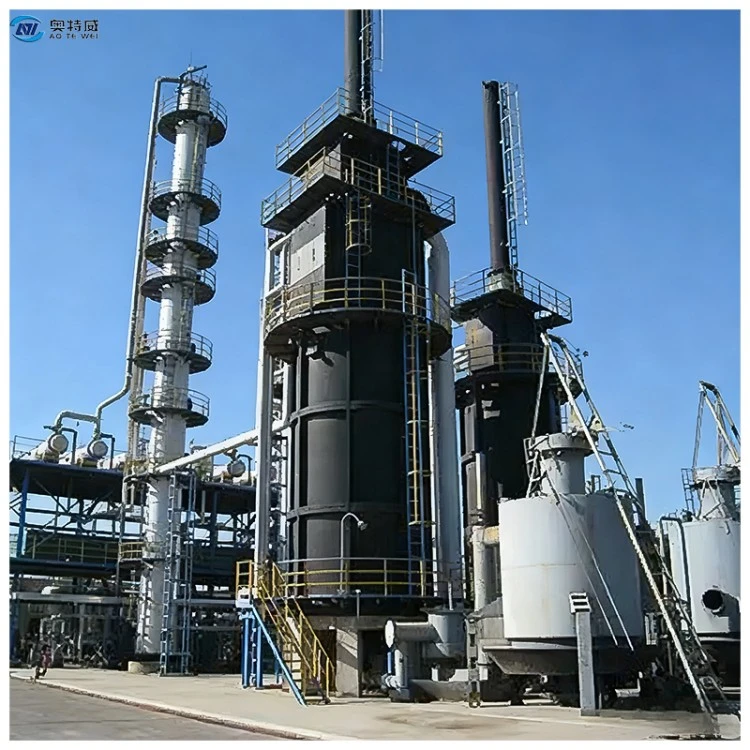
Adopting multi-column series layout to separate multiple components with different boiling points sequentially. It enables continuous feeding and continuous discharging. Different from batch single-reactor operation, it delivers large processing capacity and high-precision component separation.
Corrosion-resistant Column Body & Internals Selection:
Composite steel plates and corrosion-resistant liners are optional for material-contacting parts. It adapts to acidic and corrosive chemical media, reduces corrosion-caused equipment loss and extends service life.
Precise Automatic Reflux-ratio Control System:
Equipped with automatic reflux adjustment unit to accurately control reflux ratio, steadily stabilize the purity of distillate fractions and guarantee controllable indicators of chemical outputs.
Multi-stage Heat-exchange & Energy-coupling System:
Heat exchange occurs between feedstock and high-temperature distillates. Process waste heat is fully utilized to pre-heat incoming materials to cut heating energy consumption and realize internal energy coupling of the unit.
Sealed Negative-pressure Explosion-proof Process Design:
The whole system runs under fully-sealed conditions and can maintain high-vacuum operation to lower decomposition risks of heat-sensitive materials. It is fitted with explosion-proof electrical components, flame arrestors and tail-gas absorption units to satisfy safety specifications for chemical-industry scenarios.
Advantage
Large-capacity Continuous Processing:
Realizes 24-hour non-stop production without frequent start-stop, charging and discharging. Suitable for large-scale industrial-grade chemical-material treatment with lower processing cost per unit feedstock.
Controllable Product Purity & Simultaneous Multi-component Recovery:
Multiple qualified distillate products can be obtained simultaneously. Not only main products are recovered, but also by-products can be recycled for resource utilization, improving comprehensive material utilization rate.
Compatibility for Corrosive & Heat-sensitive Materials:
Material-matching selection together with negative-pressure low-temperature distillation avoids cracking and deterioration caused by high temperature. It can process chemical waste liquid and solvent mixtures which cannot be handled by ordinary distillation equipment.
High-level Customized Solutions:
Process simulation calculation is carried out according to customers' feedstock composition, target purity and capacity requirements. Column vessels and heat-exchange systems are designed in a targeted manner to fit diverse chemical-recovery projects.
Application Scenarios
- Separation & Processing of Petrochemical By-products: Perform component cutting for heavy-duty petrochemical by-products, separate different fractions to yield industrial-grade oil and chemical intermediates.
- Resource Utilization of Fine-chemical Waste Liquid: Distill and separate mixed waste liquid generated from fine-chemical production, recover valuable components and dispose of residual residues in compliance with regulations.
- Resource-oriented Unit for Hazardous-waste Disposal Centers: Serve as core equipment for hazardous-waste treatment enterprises. It processes various liquid chemical hazardous waste and separates recyclable components for reuse.
Packing & Shipping
The unit is shipped in modular form by process unit. Large pressure-vessel components such as distillation column sections, heat exchangers and storage tanks are treated with sandblasting and anti-corrosion coating, then firmly secured inside 40HQ, FR (Flat-Rack) or OT (Open-Top) containers. Explosion-proof instruments, DCS control cabinets, valves and pipe fittings are packed in shock-proof, moisture-proof and vacuum-sealed wooden cases. Packing list, equipment dimension-and-weight sheets, process PID drawings, general-layout drawings, pressure-vessel certificates and full set of customs-clearance documents are available. Trade terms including EXW, FOB and CIF are supported to guarantee intact cross-border ocean transportation.
FAQ
Q1: What materials can the chemical distillation plant process?
A: It is applicable to various mixed organic solvents, heavy duty petrochemical materials, chemical waste liquids, etc. Corrosion resistant materials can be customized for corrosive feedstock; negative pressure low temperature process is adopted for heat sensitive materials. A pre treatment unit shall be added for materials with high solid content.
Q2: Can the purity of output materials be guaranteed?
A: Component separation is achieved through selection of column internals and automatic reflux ratio control system. Actual purity depends on feedstock composition and process design. Process simulation can be completed combined with pilot scale test data in early stage work to lock product indicators.
Q3: How many operators are required for the continuous chemical distillation plant?
A: It adopts DCS remote centralized control. 2 3 operators per shift are sufficient under normal operation, mainly responsible for central control monitoring and on site inspection with high automation level.
Q4: What is the service life for equipment processing corrosive materials?
A: Corresponding materials are selected according to the corrosion characteristics of feedstock. The main equipment can run stably for many years under regular maintenance. Spare parts list for vulnerable components will be provided.
Q5: What preparations are required in the early stage of the project?
A: Test reports of raw materials to be treated (composition, boiling point, pH value, solid content) shall be provided. We will complete process simulation calculation and then deliver equipment proposals together with plant layout suggestions.
Company Profile & Production
Shangqiu Aotewei Environmental Protection Equipment Co., Ltd. is located in Shangqiu, Henan Province. It is a comprehensive environmental-protection equipment enterprise integrating R&D, design, production, installation, commissioning, sales and after-sales service.
Our main products include continuous-type and batch-type pyrolysis equipment for waste tyres, waste plastics, oil sludge and other waste resources, as well as waste-oil distillation, chemical distillation and pilot-scale test units. Supporting systems including desulfurization, dust removal, deodorization, denitrification, carbon-black collection and tail-gas absorption are also available.
We have 5 senior technicians, 8 engineers and more than 70 professional-technical personnel. We possess complete R&D and engineering capabilities covering lab-scale, pilot-scale and large-scale industrial chemical distillation equipment. We strictly follow pressure-vessel manufacturing standards and quality-control systems, and are an innovative enterprise taking the lead in adopting new technologies such as zirconium-aluminum insulation modules in the industry.
Our heavy-duty manufacturing workshop is equipped with automatic plate-rolling, welding, heat-treatment and non-destructive-testing facilities. Strict quality inspection is implemented for all pressure-vessel components. Up to now, we have more than 10,000 clients and our products are exported to 32 countries and regions worldwide. We have won extensive recognition from domestic and overseas customers with reliable product quality and complete after-sales service, and keep boosting the resource recovery of global chemical waste liquid and the development of green circular economy.
Hot Tags: chemical distillation plant, China chemical distillation plant manufacturers, suppliers, factory



