
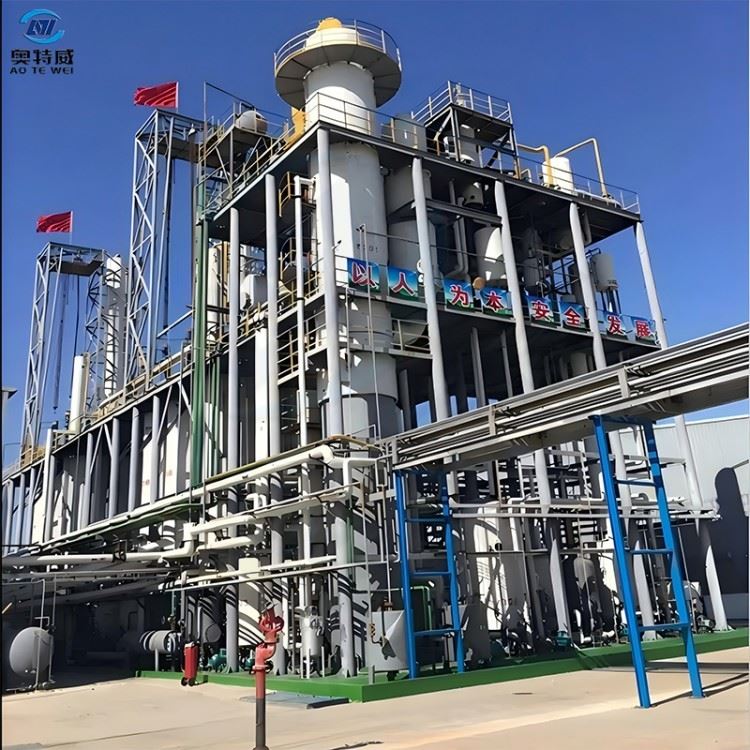
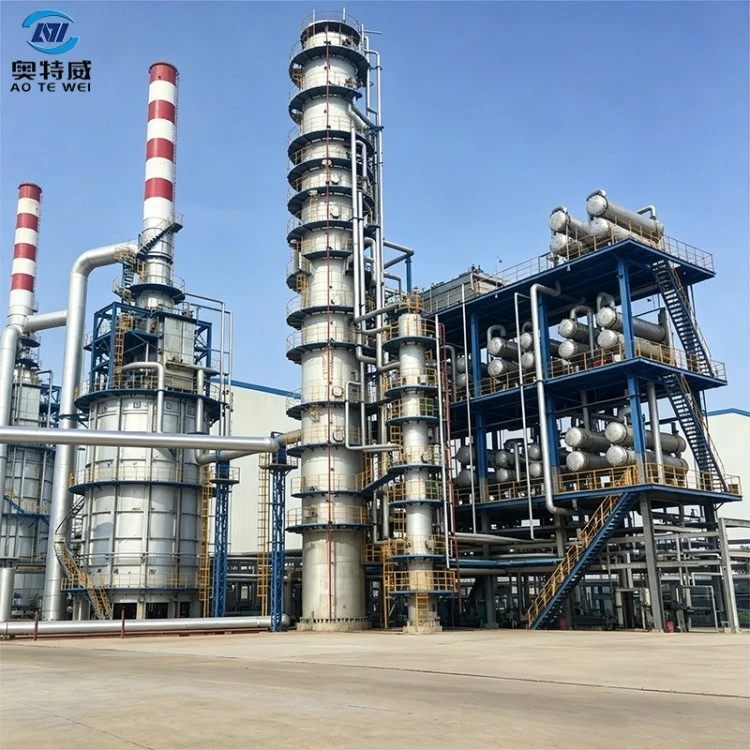
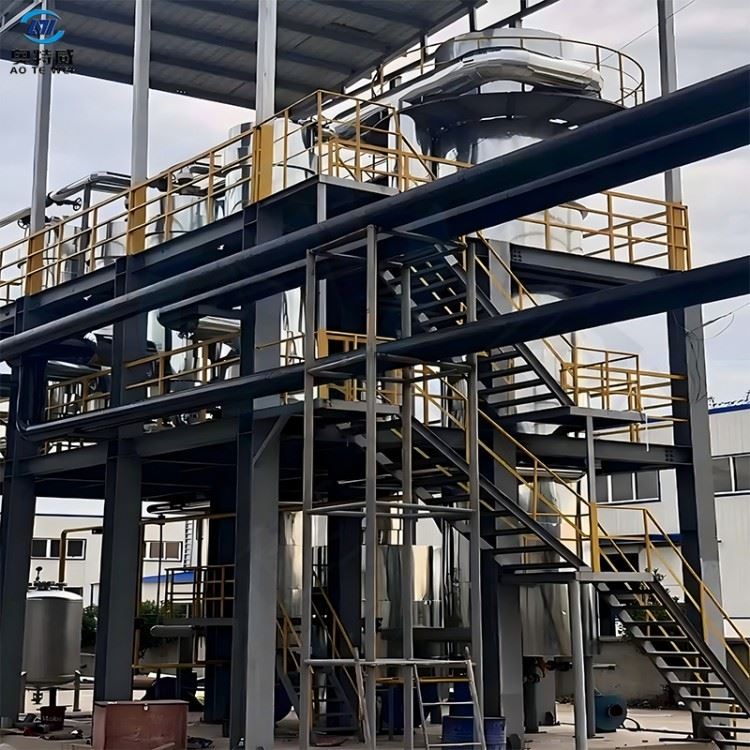
Shangqiu Aotewei Environmental Protection Equipment Co., Ltd. is one of the leading manufacturers and suppliers of used oil distillation plant in China. We are committed to providing high quality customized products with competitive price. If you're going to buy ISO certified used oil distillation plant, welcome to get quotation from our factory.
Product Name
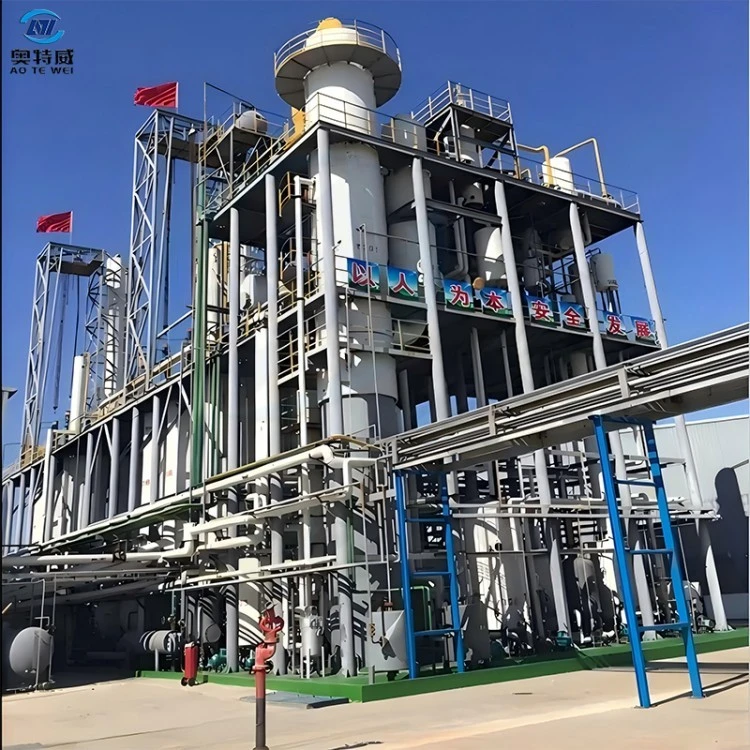
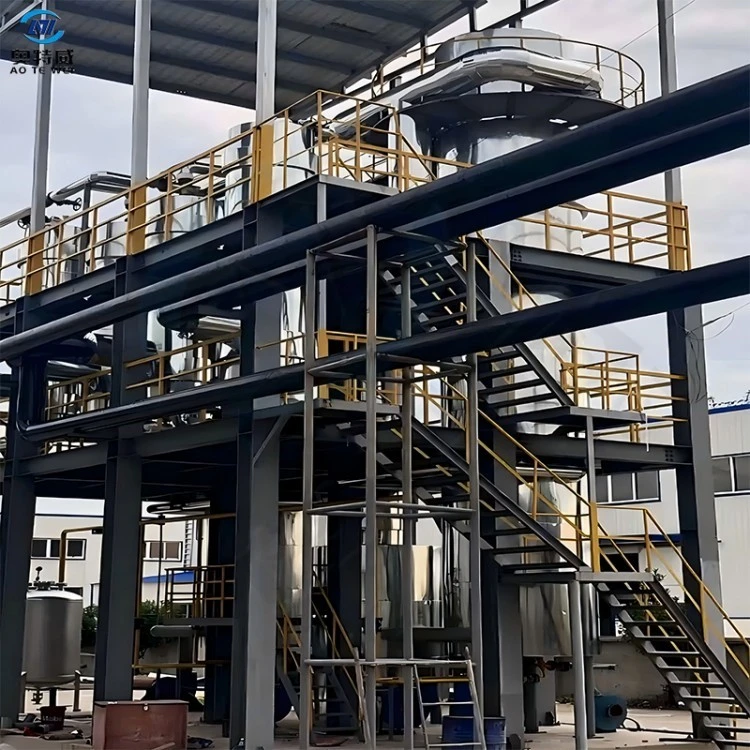
Used Oil Distillation Plant Distillation and refining unit featured with horizontal rotary distillation technology. It purifies waste engine oil, waste lubricating oil, pyrolysis oil into high-quality fuel oil. Adopting indirect heating and multi-stage condensation for stable oil yield, it is widely applied in industrial regeneration of waste oil resources.
| Technical Parameter of the Pyrolysis plant | |||
| 1 | Suitable Raw Materials | Waste Engine Oil, Fuel Oil, Crude Oil | Waste Engine Oil, Fuel Oil, Crude Oil |
| 2 | Structure | Horizontal Rotation Type | Horizontal Rotation Type |
| 3 | Reactor Size | φ2600×6600mm φ2800×8000mm φ3000×8800mm |
φ1500×2000mm φ1800×4000mm φ2000×600mm |
| 4 | Work Pressure | Normal Pressure | Normal Pressure |
| 5 | Oil Yield | 85%~95% | 85%~95% |
| 6 | Work Pressure | Normal Pressure | Normal Pressure |
| 7 | Power | 15-25kw/H | 15-25kw/H |
| 8 | Heating Method | Indirect Heating | Indirect Heating |
| 9 | Type of Installation | Without Foundation | Without Foundation |
| 10 | Cooling Method | Cycling Water | Cycling Water |
| 11 | Noise dB (A) | ≤ 85 | ≤ 85 |
| 12 | Cooling Method | Cycling Water | Cycling Water |
| 13 | End Product | Non-standard Diesel Oil | Non-standard Diesel Oil |
| 14 | Manpower | 4-6/shift | 2-4/shift |
Features
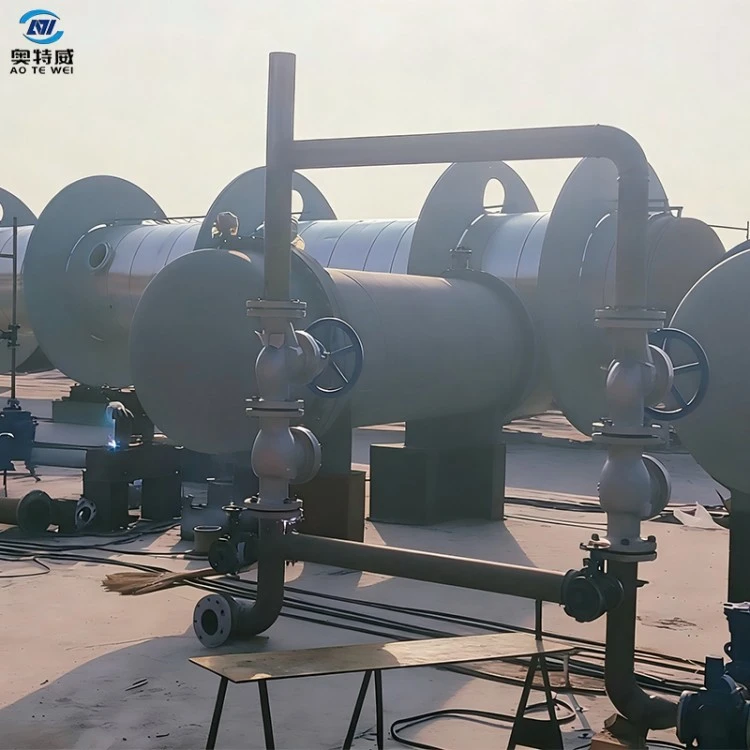
Large-volume Horizontal Rotary Distillation Reactor:
Fabricated from high-quality boiler steel plate. It features large and evenly heated surface. With rotary structure for continuous material agitation, it effectively prevents local overheating and coking for thorough distillation.
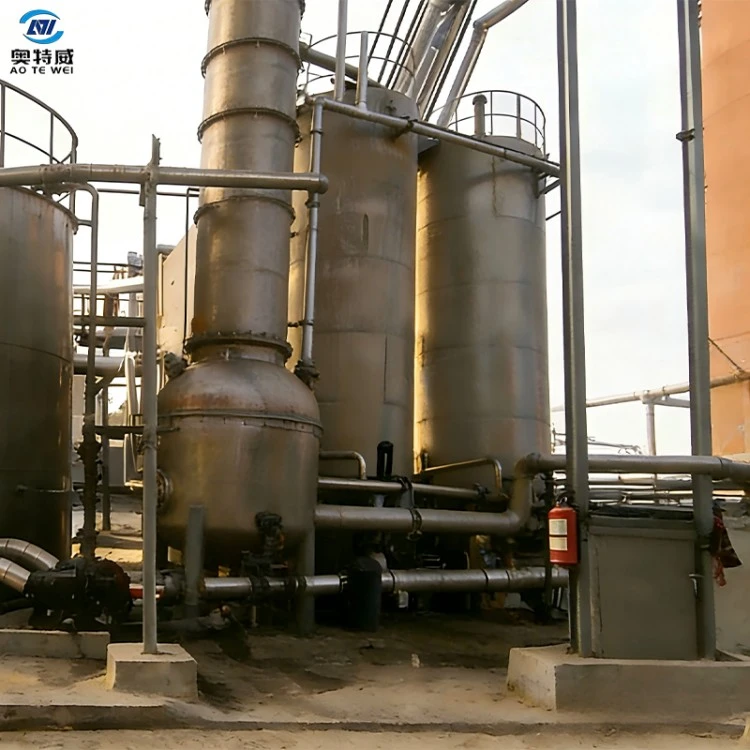
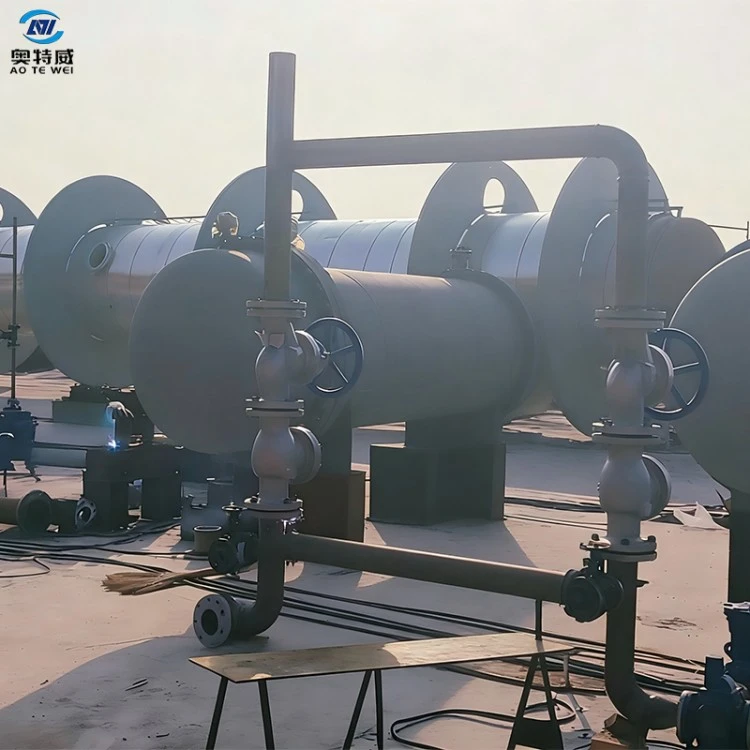
Multi-stage Large-diameter Tubular Condensation System:
Condenser adopts large-diameter tubular structure with sufficient heat-exchange area for fast and full liquefaction of oil-gas. Multi-stage series connection enables fractional collection, greatly improving oil recovery rate and condensation efficiency.
Flexible Switch between Atmospheric and Vacuum Operation:
Supports both atmospheric and negative-pressure distillation modes. Operating pressure can be adjusted according to feedstock properties to lower oil boiling point and reduce cracking, so as to obtain premium oil under mild conditions.
Waste-heat Recovery Heating System:
Recovers heat from flue gas to pre-heat raw oil. Non-condensable gas generated from distillation is reused as supplementary heat source. It realizes thermal energy recycling and cuts fuel consumption and operating cost.
Skid-mounted Integrated for Easy Installation:
Core systems are integrated on skid-mounted base or fixed foundation. Compact footprint enables quick commissioning after on-site wiring. Both foundation-required and foundation-free installation options are available.
Centralized Control with Safety Interlock:
Integrated monitoring for temperature, pressure and liquid level. Auto-alarm and interlock protection are triggered upon over-temperature and over-pressure. Intuitive operation reduces manual attendance and ensures safe operation.
Advantage
Excellent Oil Recovery Rate:
Actual measured product oil recovery reaches 85%-95% with little residue output, directly boosting profit margin and return on investment per ton of feedstock.
Low Energy Consumption & Good Economy:
Indirect heating combined with waste-heat recovery and non-condensable gas reuse greatly reduces dependence on external fuel, delivering prominent cost advantages for long-term continuous operation.
Stable Product Quality: Distilled oil features clear appearance, high flash point and low impurity content. It can be directly used as fuel for industrial boilers, burners and generators, ready for commercial sales.
Durable Equipment & Easy Maintenance:
Key components adopt high-temperature and corrosion-resistant materials. Robust condensation and heat-exchange structures extend maintenance cycle and effectively lower later-stage operating expenses.
Complete Specifications & Flexible Adaptation:
Multiple reactor sizes for selection. Customization based on production capacity and feedstock characteristics is supported, meeting demands from small-scale processing to large-volume production.
Full-process Service Support: One-stop service covering design & manufacturing, installation & commissioning, operation training and after-sales support. On-site engineer service is available to facilitate fast commissioning.
Application Scenarios
- Centralized Waste Engine Oil Recycling Station: Distill and refine waste engine oil generated from automobile and machinery maintenance to produce usable fuel oil on-site for waste oil reuse.
- Small-scale Waste-oil Regeneration Plant: Large-volume processing of waste engine oil and waste lubricating oil. Distilled non-standard diesel and fuel oil are sold for considerable economic returns.
- Pyrolysis Oil Upgrading Project: Matched with pyrolysis units for further distillation and purification of crude pyrolysis oil to improve oil quality and added value.
- In-house Waste Oil Treatment for Factories: Supply on-site waste oil distillation and recovery units for factories, mines and shipyards. It cuts hazardous waste disposal cost and supplements internal fuel supply.
- Oil Blending & Refining Unit: Uniformly distill and refine waste oil from various sources, and blend into industrial fuel oil with stable calorific value and qualified quality.
Packing & Shipping
Equipment is delivered in modular split shipment. Functional units including distillation reactor, condenser and electric control cabinet are shipped separately. Large reactors are treated with rust removal and anti-corrosion coating, and firmly secured inside 40HQ, FR (Flat-Rack) or OT (Open-Top) containers. Precision instruments, sensors and control cabinets are packed in shock-resistant, vacuum-sealed waterproof wooden cases. Packing list, equipment dimension-weight sheet, general layout drawing and full set of customs-clearance documents are provided. Trade terms of EXW, FOB, CIF are supported to guarantee safe and intact global ocean transportation.
FAQ
Q1: What types of oil can this plant process?
A: It can handle waste engine oil, waste lubricating oil, pyrolysis oil and various waste mineral oil. Distillation conditions can be adjusted for different feedstock, and customized specifications are available.
Q2: What about the quality of final distilled oil?
A: After distillation and purification, oil is clear and transparent with high flash point and few impurities. It can be directly used as industrial fuel or sold commercially.
Q3: What is the oil recovery rate?
A: Under normal operating conditions, product oil recovery reaches 85% 95% with low residue output and high comprehensive benefits.
Q4: How many operators are needed for the complete plant?
A: Equipped with centralized control system. Around 2 4 operators per shift are sufficient for central monitoring and on site inspection with easy operation.
Q5: Does the plant consume large energy?
A: Indirect heating together with waste heat recovery and non condensable gas reuse realizes high efficiency energy utilization, greatly cutting external fuel consumption for favorable operating economy.
Company Profile & Production
Shangqiu Aotewei Environmental Protection Equipment Co., Ltd. is located in Shangqiu, Henan Province. It is a comprehensive environmental-protection enterprise integrating R&D, design, production, installation, commissioning, sales and after-sales service.
Our main products include continuous and batch pyrolysis equipment for waste tyres, waste plastics, oil sludge and other waste resources, as well as used oil distillation and waste oil recycling regeneration plants. Supporting systems such as desulfurization, dust removal, deodorization, denitrification and carbon black collection are also available.
We have 5 senior technicians, 8 engineers and more than 70 professional technical personnel with strong scientific research and engineering capabilities. We strictly comply with industrial manufacturing standards and quality-control systems. As an innovative enterprise, we take the lead in applying new technologies such as zirconium-aluminum insulation modules.
Our heavy-duty workshop is equipped with automatic plate-rolling, welding, heat-treatment and non-destructive-testing equipment, with strict inspection for pressure-vessel components. Up to now, we own over 10,000 clients and our products are exported to 32 countries and regions worldwide. We have gained extensive trust from domestic and overseas customers with reliable quality and complete after-sales service, and keep promoting the development of global green circular economy.
Hot Tags: used oil distillation plant, China used oil distillation plant manufacturers, suppliers, factory


