
Shangqiu Aotewei Environmental Protection Equipment Co., Ltd. is one of the leading manufacturers and suppliers of tyre pyrolysis plant in China. We are committed to providing high quality customized products with competitive price. If you're going to buy ISO certified tyre pyrolysis plant, welcome to get quotation from our factory.
Products Description
Tyre Pyrolysis Plant
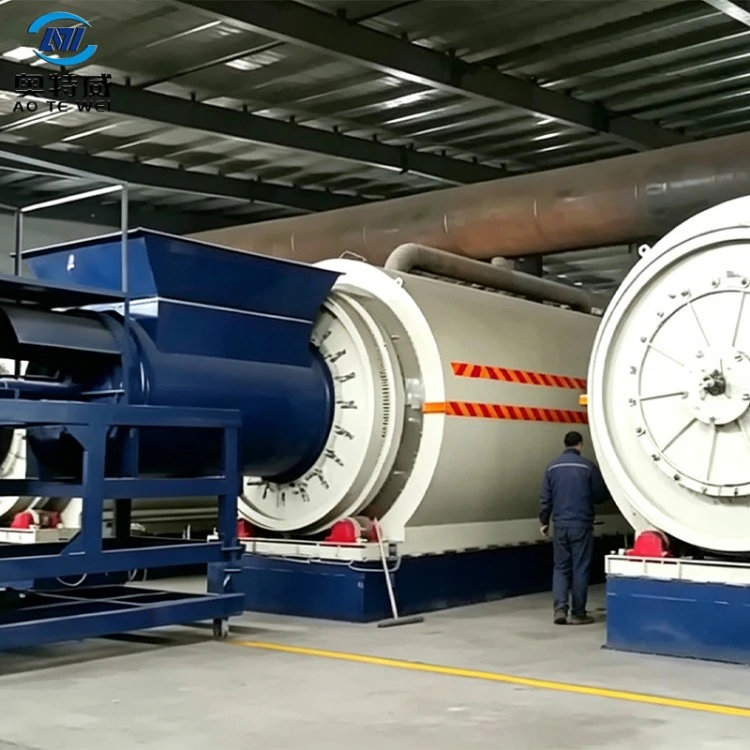
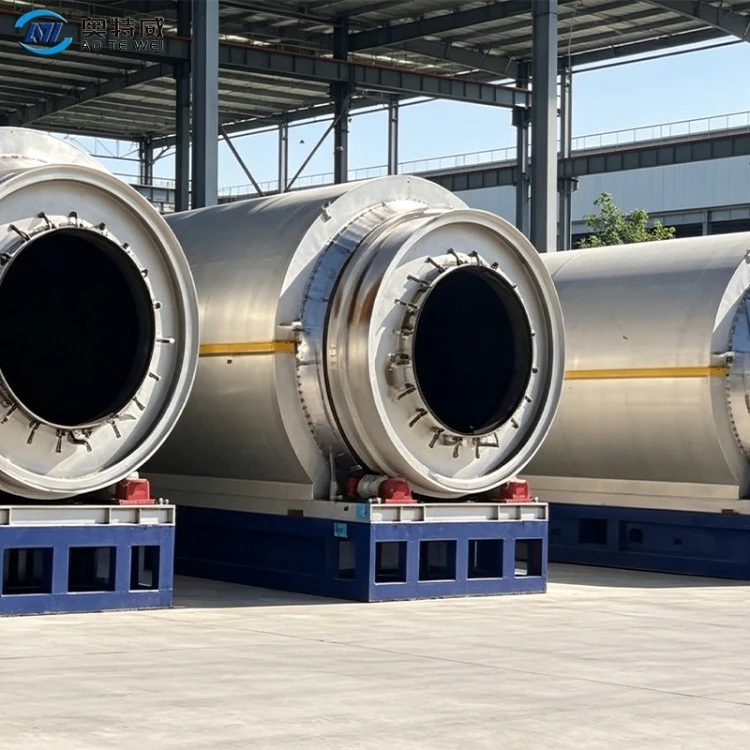
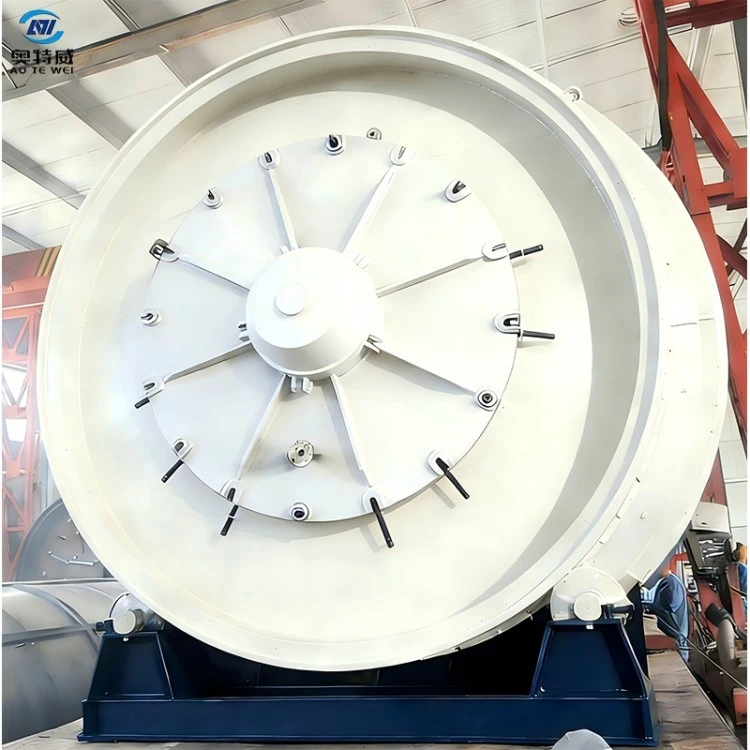
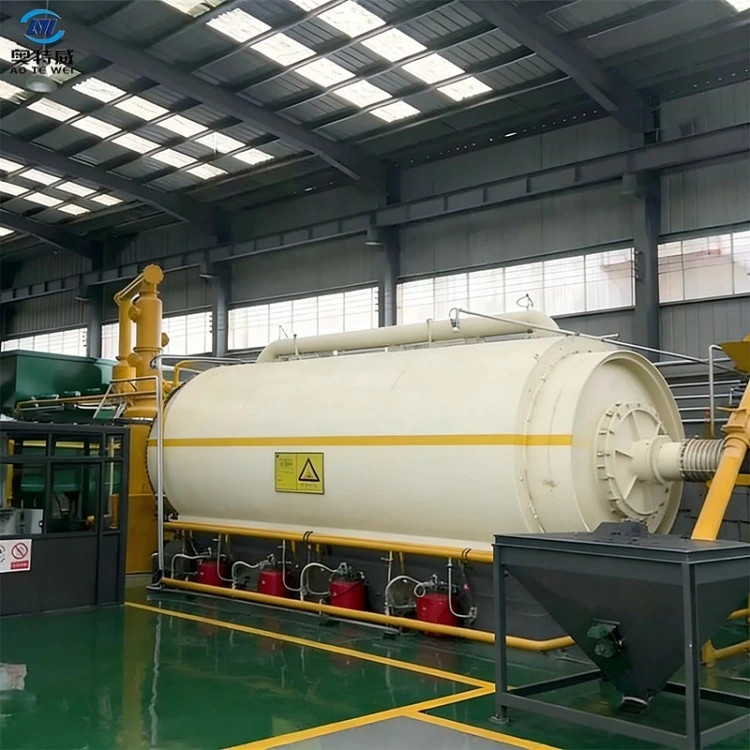
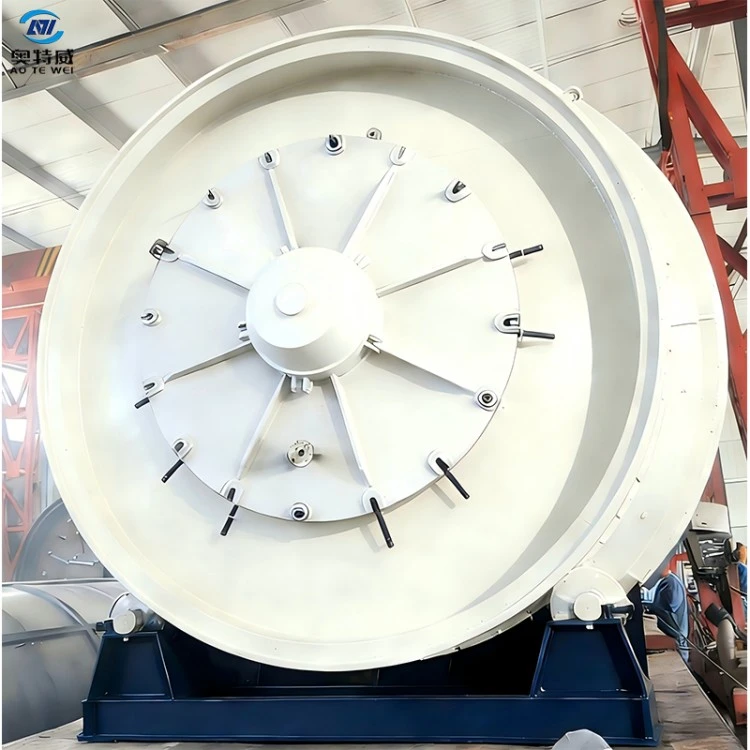
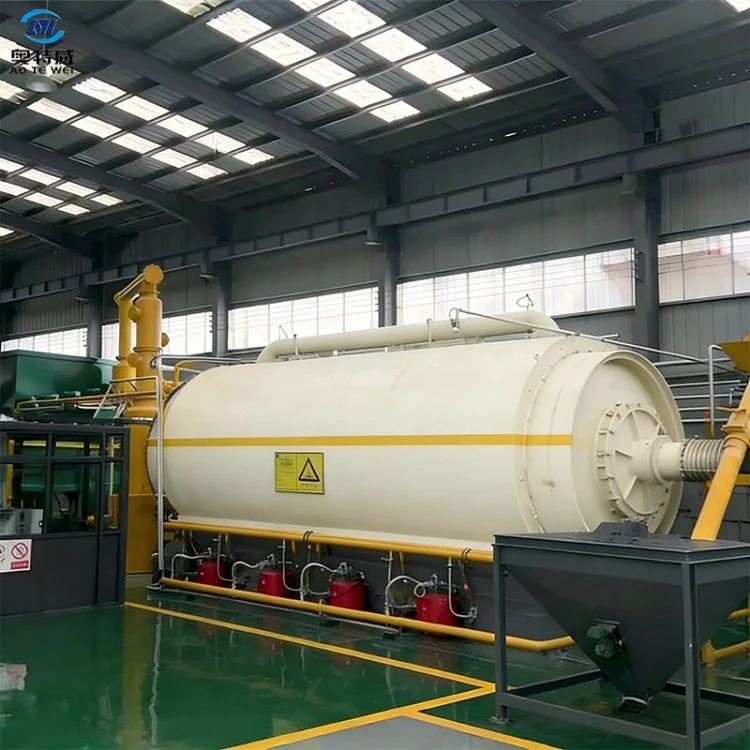
The Tyre Pyrolysis Plant is a dedicated batch-type pyrolysis equipment developed by Aotewei for large-scale waste tyre recycling. Optimized for the cross-linked macromolecular structure and high rubber content of waste tyres, it efficiently converts used passenger-car tyres, truck tyres and off-road tyres into four high-value recyclable outputs: pyrolysis oil, carbon black, steel wire and combustible gas. Featuring large-door whole-tyre feeding design, it eliminates complex pre-shredding requirements. Combined with synchronous gas recycling-combustion system and high-efficiency condensation modules, it realizes full-component recovery of tyre resources. As core equipment for reduction, harmless treatment and resource utilization within the tyre recycling chain, it is widely adopted by tyre recyclers, solid-waste disposal centres and eco-energy projects.
Price Note: Quotation is subject to steel-market fluctuation, configuration grade, processing capacity and international exchange rates. The reference price for the standard 10-ton-per-day tyre pyrolysis plant is USD 56,000 / set (excluding sea freight, import duties and on-site installation & commissioning costs).
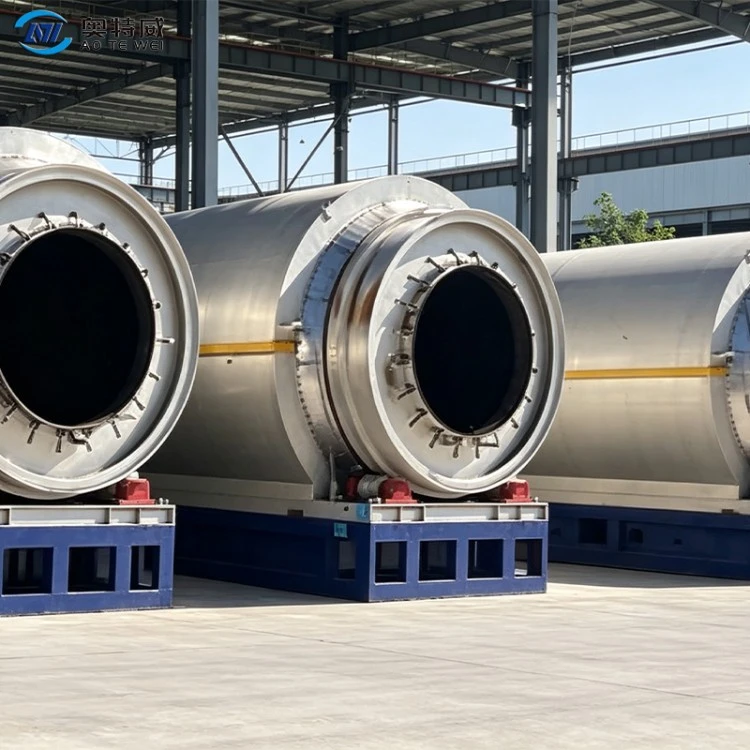
| Technical Parameter of the Pyrolysis plant | |||
| 1 | Suitable Raw Materials | Rubber/Plastic Products etc | Rubber/Plastic Products etc |
| 2 | Structure | Horizontal Rotation Type | Horizontal Rotation Type |
| 3 | Reactor Size | φ2600×6600mm φ2800×8000mm φ3000×8800mm |
φ1500×2000mm φ1800×4000mm φ2000×600mm |
| 4 | Capacity for One Batch | 8-10Mt; 12-15Mt; 18-20Mt | 1Mt; 3Mt; 5Mt |
| 5 | Oil Yield from Tyres | 38%~45% | 38%~45% |
| 6 | Work Pressure | Normal Pressure | Normal Pressure |
| 7 | Reactor Rotation Speed | 0.4R/M | 0.4R/M |
| 8 | Fuels Choice | Coal, Wood, Gas, Oil | Coal, Wood, Gas, Oil |
| 9 | Power | 15~22kw/h | 8~15kw/h |
| 10 | Cooling Method | Cycling Water | Cycling Water |
| 11 | Type of Drive | External Annular Gear | External Annular Gear |
| 12 | Heating Method | Direct Heating | Direct Heating |
| 13 | Type of Installation | Without Foundation | With Foundation / Integrated Base |
| 14 | Noise dB (A) | ≤ 85 | ≤ 85 |
| 15 | Operating Mode | Intermittent Operation | Intermittent Operation |
| 16 | Total Weight (MT) | 25~50 | 10~25 |
Features
① Large-door whole-tyre feeding
Adopts large-diameter quick-open furnace door. Whole tyres or roughly-cut tyre blocks can be fed directly without heavy pre-shredding equipment. Bolt quick-lock sealing ensures easy opening-closing and effective prevention of oil-gas leakage.
② Tyre-specific staged-temperature pyrolysis with stable product yields
Under optimized 380-420 °C working temperature range, rubber gets fully cracked while coking and heavy-oil generation are suppressed. Typical yields: 40-48 % pyrolysis oil, 30-35 % carbon black, 12-15 % steel wire. Comprehensive material utilization rate reaches nearly 100 %.
③ Combustible-gas recycling combustion for high energy self-sufficiency
Purified non-condensable gas from pyrolysis is fed back to the combustion chamber as fuel, achieving over 90 % energy self-supply. Only small-volume external fuel is needed for cold-furnace ignition. Equipped with surplus-gas combustion chamber and safety vent for reliable operation and lower fuel expenses.
④ Modular multi-stage tubular condenser for thorough oil-gas liquefaction
Double-inlet & double-outlet condenser is optimized for tyre-pyrolysis oil-gas to improve oil recovery. Exposed flange connections allow easy oil-stain cleaning and pipeline inspection without complicated disassembly for convenient maintenance.
⑤ Full-process sealed negative-pressure design plus standard tail-gas treatment for low-pollution emission
Full-process negative-pressure sealing and flame-arrest protection prevent oil-gas leakage. Integrated spray dust-removal & desulfurization unit treats flue gas for smokeless and low-odor operation, meeting basic environmental-acceptance requirements.
Advantages
① Full-component tyre recovery for maximized product value
Waste tyres are converted into four usable products: pyrolysis oil, carbon black, steel wire and combustible gas with no secondary solid waste generated. Pyrolysis oil can be used as industrial fuel or further refined. Carbon black and steel wire are marketable end-products. Recycled combustible gas supplies heating for the plant. Each ton of feedstock brings considerable profit with short project payback period.
② Whole-tyre feeding cuts capital & operating costs
Whole tyres can be directly loaded, removing the need for extra large tyre-shredding equipment. It saves power consumption and wearing-part replacement costs caused by shredding procedures. Compared with pyrolysis units requiring fine shredding, this solution lowers upfront investment and daily operating expenditure, well-suited for large-scale tyre-recycling projects.
③ Proven reliable process with low failure rate
The mature batch-type pyrolysis technology has been verified in numerous real-world projects. The main reactor is made of Q345R pressure-vessel steel plate with standardized welding procedures. Targeted anti-coking structure reduces breakdown risks. Under normal working conditions, the reactor service life can reach 5 years to support long-term continuous production.
④ Easy operation & low labour requirement
Simplified electric-control system combines push-buttons and digital displays. Key parameters are monitored in real-time with over-temperature alarm function. Complex full-automatic interlock logics are omitted. Ordinary workers can master complete production workflows after short-term training, removing the need for highly-paid professional technicians and cutting labour costs.
⑤ Flexible configuration to match diverse project demands Standard and high-end versions are optional for different client requirements. High-end options include zirconium-aluminum insulation modules, split-type supporting rollers, 316L sealing baffles and upgraded tail-gas-treatment assemblies. These upgrades help boost production capacity, extend equipment service life and satisfy strict environmental-protection standards for various budgets and project conditions.
Application Scenarios
- Core equipment for waste-tyre recycling enterprises: Professional tyre recyclers convert collected waste tyres into high-value products via pyrolysis. It helps enterprises upgrade from simple waste collection & resale to resource-oriented finished-product manufacturing, greatly improving profitability and market competitiveness.
- Waste-disposal project for tyre manufacturers & rubber factories: Tyre and rubber product plants treat in-house waste rubber materials, defective tyres and production trimmings. It relieves corporate environmental-disposal pressure. Recovered pyrolysis oil and combustible gas can be reused for factory boilers and equipment to reduce energy procurement costs.
- Centralized-disposal site for auto-repair & tyre-retail chains: Multiple regional auto-repair and tyre-shop partners build joint pyrolysis stations to centrally process waste tyres replaced from outlets. Waste is turned into saleable goods, eliminating third-party waste-tyre-disposal service fees and generating extra revenue.
- Raw-material supporting project for carbon-black & reclaimed-rubber manufacturers: Supplies pyrolysis-derived carbon black for carbon-black and reclaimed-rubber factories. The output carbon black can serve directly as rubber-reinforcing filler for reclaimed-rubber production, lowering clients' raw-material costs and realizing industrial linkage between tyre recycling and carbon-black / reclaimed-rubber production.
Packing & Shipping
Packing Method:
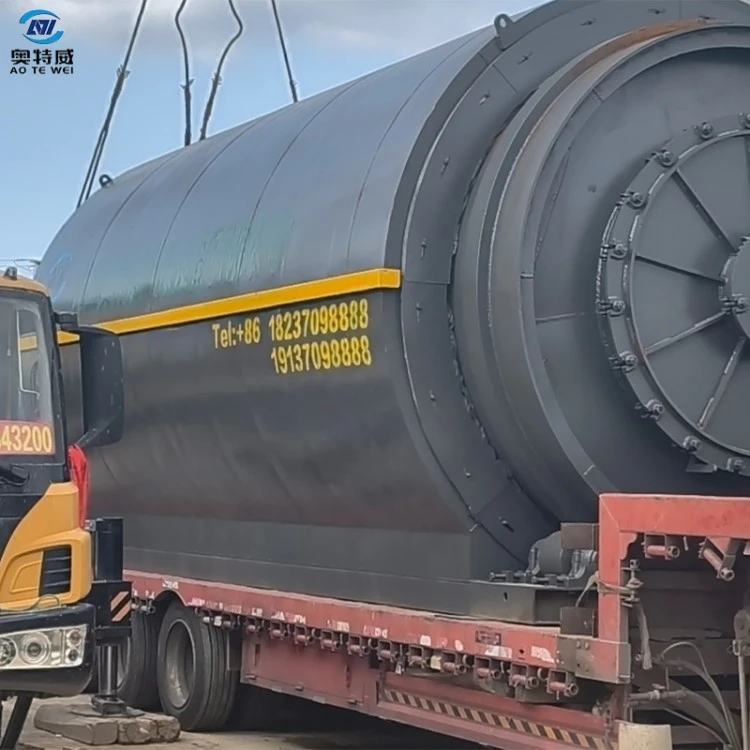
Main heavy-duty components receive anti-rust paint and are wrapped with waterproof tarpaulin. Lifting lugs and transport locking structures are pre-reserved. Precision accessories including electric-control cabinet, instruments and valves are packed in shock-proof and moisture-proof wooden cases. Pipes, flanges, sealing gaskets, tools and wearing-part spares are sorted and palletized. Bilingual operation manuals, assembly sketches and packing list are provided with goods.
Shipping Method:
The standard 10-ton-per-day tyre pyrolysis plant is split and loaded into 1-2 ×40HQ containers for sea export. Large custom-built equipment can be shipped in modular containers or by break-bulk vessel. Inland shipments can be delivered directly to site via flat-bed trucks.
Delivery Lead Time:
For standard configurations, production and no-load testing will be finished within 60-80 working days upon receipt of advance payment before shipment. Lead time will be extended for high-end or custom-tailored models. Real-product photos and test videos will be delivered pre-shipment to assist customers with site preparation.
FAQ
Q1: What is the standard daily processing capacity? Can higher capacity be customized?
A: The standard model is designed for 10 tons per day calculated on waste tyre basis. Custom built variants of 15 tons and 20 tons per day are available upon request. For larger throughput, our continuous flow tyre pyrolysis plant or parallel connected batch units are recommended.
Q2: What raw-material requirements apply to waste tyres? Is shredding necessary?
A: Equipped with large furnace door, the unit accepts whole tyres or roughly cut tyre blocks without fine shredding. It is recommended to remove bulky foreign objects and sediment in advance to improve pyrolysis efficiency and product quality.
Q3: What product yields can be obtained per ton of waste tyre?
A: Yields vary according to tyre categories and rubber content. For regular passenger car and truck tyres: pyrolysis oil 40% 48 %, carbon black 30% 35 %, steel wire 12% 15 %, combustible gas 8% 10 %. Comprehensive material utilization rate is nearly 100 %.
Q4: Can the equipment pass local environmental protection inspections?
A: Adopting full process sealed negative pressure pyrolysis plus integrated desulfurization dust removal tail gas treatment unit, it achieves smokeless low odor operation and meets basic emission standards for small and medium sized projects. Customers shall complete EIA filing in accordance with local regulations. Upgraded advanced waste gas treatment assemblies (activated carbon adsorption, catalytic combustion, etc.) are optional for regions with stringent emission requirements.
Company Profile & Production Capacity
Shangqiu Aotewei Environmental Equipment Co., Ltd. is an R&D-oriented manufacturer integrating equipment development, production and after-sales service, located in Liangyuan District, Shangqiu, Henan Province. With more than ten-year experience in solid-waste pyrolysis for waste tyres, waste plastics, oil sludge and other feedstocks, we are among China's early enterprises realizing localized mass production of pyrolysis equipment.
Our technical team consists of engineers and senior technicians. We have developed multiple proprietary technologies covering reactor structure, feeding-slag-discharge system, burner unit and combustible-gas recovery. We are the first player in the industry to independently develop, mass-produce and provide quality-guaranteed gas-storage bags. Multiple technical improvements have boosted equipment efficiency and on-site working conditions.
Our standardized manufacturing workshop is fully furnished with complete sets of facilities for pressure-vessel rolling, welding, non-destructive testing and complete-machine commissioning. The whole production chain from raw-material cutting, machining, welding, assembly to final inspection is completed in-house. Our product portfolio includes five major series: batch-type pyrolysis plants, continuous pyrolysis units, distillation refining equipment, carbon-black deep-processing machines and matching auxiliaries. Annual output can reach more than 50 sets of medium-and-large-size complete lines, while small auxiliary components support fast batch delivery.
Our products are exported to over 30 countries worldwide and have served more than 10,000 domestic and overseas clients with solid market reputation. We deliver customized solutions according to on-site working conditions, local raw-material properties, environmental-protection codes and capacity targets. Our one-stop full-lifecycle services cover project planning, equipment manufacturing, installation guidance, operator training and after-sales maintenance to guarantee stable operation and profitable solid-waste-resource-recovery projects.
Hot Tags: tyre pyrolysis plant, China tyre pyrolysis plant manufacturers, suppliers, factory


