
Shangqiu Aotewei Environmental Protection Equipment Co., Ltd. is one of the leading manufacturers and suppliers of coal pyrolysis plant in China. We are committed to providing high quality customized products with competitive price. If you're going to buy ISO certified coal pyrolysis plant, welcome to get quotation from our factory.
Products Description
Low-Temperature Coal Pyrolysis Plant
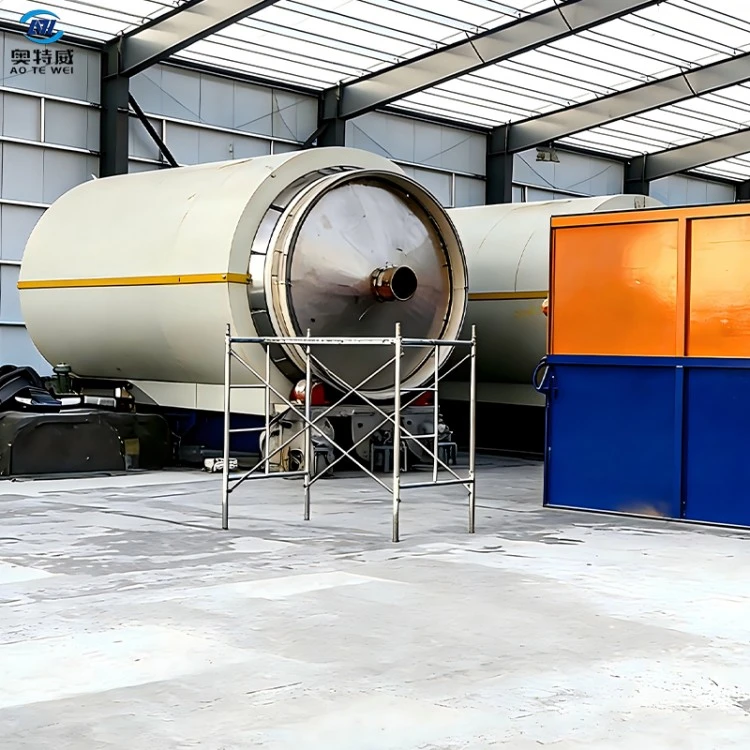
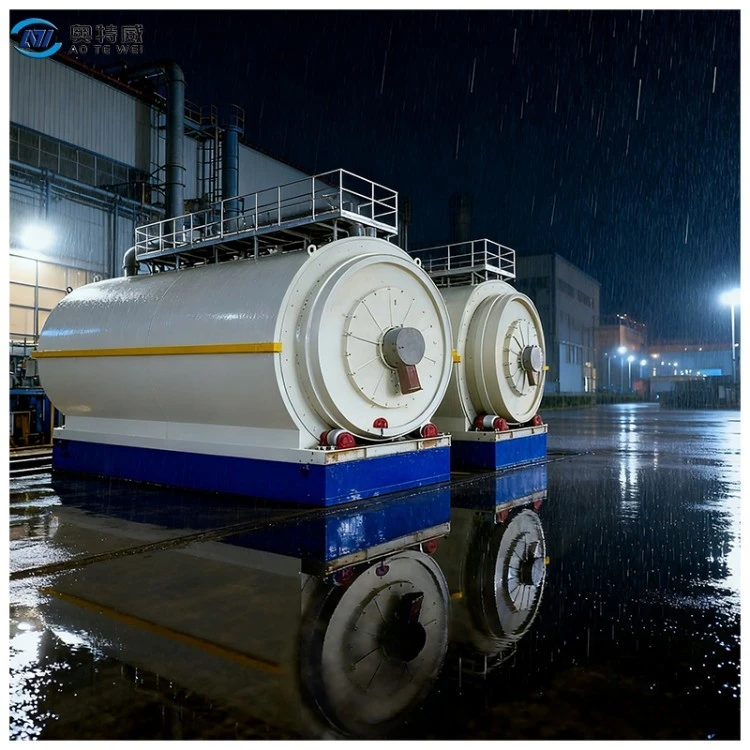
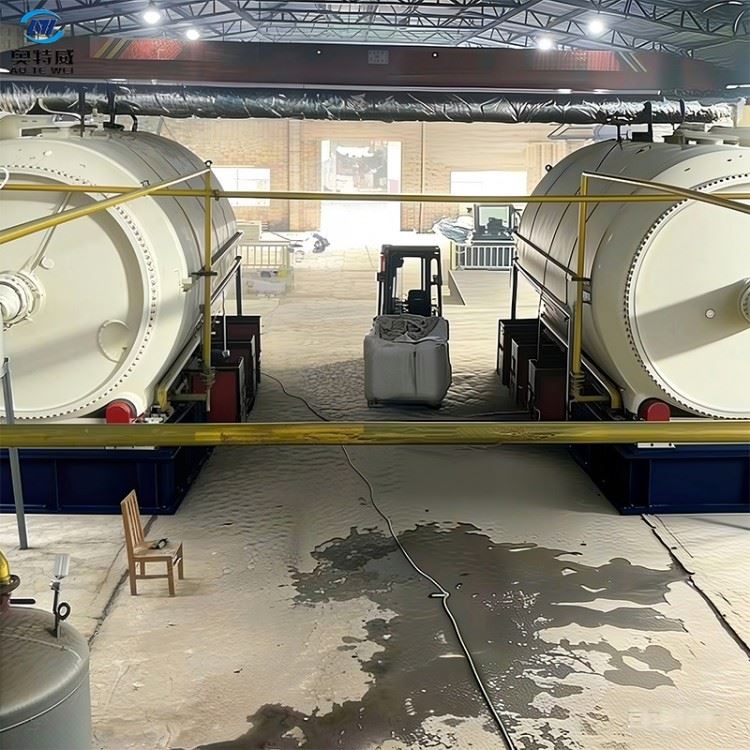
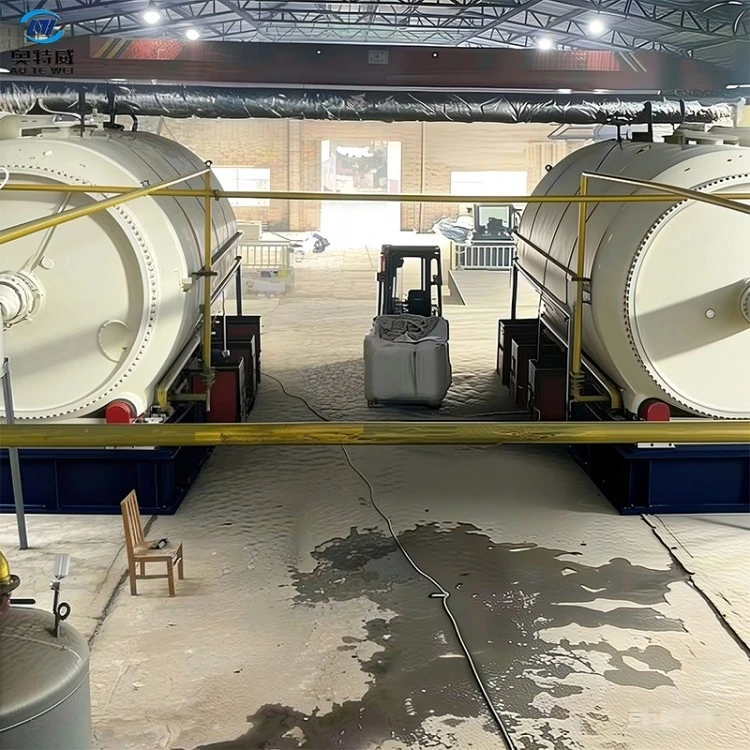
The Low-Temperature Coal Pyrolysis Plant is an independently-developed batch-type horizontal-rotary pyrolysis unit by Aotewei for low-rank coal upgrading. It is applicable to feedstocks such as lignite, bituminous coal and coal slime. Through oxygen-isolated low-temperature pyrolysis technology, raw coal is converted into coal tar, coal gas and semi-coke. It realizes co-production of multiple products to maximize coal-resource value. Flexible capacity options are available for coal-resource bases and coal-chemical demonstration projects.
Price Note: Final quotation is subject to steel cost, processing capacity, auxiliary-equipment configuration and exchange rate. Reference price for standard 10-ton-per-day model: USD 80,000 / set, excluding sea freight, import duties and on-site installation & commissioning. Custom formal quotation can be offered based on coal-quality analysis reports and project requirements.

| Technical Parameter of the Pyrolysis plant | |||
| 1 | Suitable Raw Materials | Rubber/Plastic Products etc | Rubber/Plastic Products etc |
| 2 | Structure | Horizontal Rotation Type | Horizontal Rotation Type |
| 3 | Reactor Size | φ2600×6600mm φ2800×8000mm φ3000×8800mm |
φ1500×2000mm φ1800×4000mm φ2000×600mm |
| 4 | Capacity for One Batch | 8-10Mt; 12-15Mt; 18-20Mt | 1Mt; 3Mt; 5Mt |
| 5 | Oil Yield from Tyres | 38%~45% | 38%~45% |
| 6 | Work Pressure | Normal Pressure | Normal Pressure |
| 7 | Reactor Rotation Speed | 0.4R/M | 0.4R/M |
| 8 | Fuels Choice | Coal, Wood, Gas, Oil | Coal, Wood, Gas, Oil |
| 9 | Power | 15~22kw/h | 8~15kw/h |
| 10 | Cooling Method | Cycling Water | Cycling Water |
| 11 | Type of Drive | External Annular Gear | External Annular Gear |
| 12 | Heating Method | Direct Heating | Direct Heating |
| 13 | Type of Installation | Without Foundation | With Foundation / Integrated Base |
| 14 | Noise dB (A) | ≤ 85 | ≤ 85 |
| 15 | Operating Mode | Intermittent Operation | Intermittent Operation |
| 16 | Total Weight (MT) | 25~50 | 10~25 |
Features
① Low-temperature oxygen-isolated pyrolysis for guaranteed product quality
Adopts strict oxygen-isolated low-temperature pyrolysis process to prevent excessive cracking of coal-tar components. It produces high-quality coal tar and high-strength semi-coke and realizes graded conversion of organic substances in coal.
② Horizontal rotary reactor for even material heating
Horizontal rotary reactor with external-gear-ring transmission. Coal particles keep tumbling during pyrolysis to avoid local over-heating and caking. It accepts coal feedstock with wide particle-size range and delivers stable pyrolysis performance.
③ Multi-stage composite condensation system for high tar-recovery rate
Integrates cyclone dust-removal, tubular condensation and oil-mist-capture units. It effectively separates coal dust from volatile matters, reduces tar carry-over loss, improves coal-tar yield and delivers low-ash clean-grade tar.
④ Independent coal-gas circulating combustion system for energy recovery
Purified pyrolysis coal gas is fed back to combustion chamber as heating fuel to greatly cut external-fuel consumption. Adjustable air-fuel ratio enables stable and controllable furnace-temperature.
⑤ Modular composite structure for flexible expandable configuration
The main reactor, dust-removal, condensation and gas-combustion modules are independently engineered. Customers may add coal crushing-screening, semi-coke cooling and deep tar-filtration modules later according to project budget and raw-coal conditions.
Advantages
① Multi-product co-production for sound comprehensive economic returns
One single unit yields three high-value outputs: coal tar, semi-coke and pyrolysis coal gas. Semi-coke can be sold for metallurgy, carbon-material production or as clean fuel. Coal tar can be further refined into heavy fuel oil. Diversified revenue mitigates market risks brought by single-product price fluctuation.
② Broad coal-type adaptability to fully utilize low-value coal resources
Compatible with lignite, long-flame coal, non-caking coal and coal slime. It upgrades low-rank coal which is hard for long-distance transport and direct combustion, and realizes on-site value-adding for coal-mine waste resources.

③ Atmospheric-pressure operation with high-level safety
The whole plant runs under atmospheric pressure without high-pressure hazards from pressure vessels. Real-time monitoring sensors for temperature, pressure and flue gas are fitted together with abnormal-alarm functions to enhance operational safety.
④ Self-produced coal-gas heating lowers operating costs
Most heat comes from combustion of self-generated pyrolysis gas. Only a small quantity of auxiliary fuel is required for initial ignition. Long-term fuel expenditure is greatly reduced compared with systems relying fully on external fuel.
⑤ Easy-to-maintain structure for extended service life The reactor is fabricated from high-temperature-resistant pressure-vessel steel plate. Key rotating components adopt wear-resistant alloy treatment. Manholes and inspection ports are reserved for convenient regular internal inspection and slag-cleaning work.
.
Application Scenarios
- Coal-mine resource-base projects: Deployed adjacent to open-pit or underground coal mines to locally process on-site low-rank coal and coal slime. Produced semi-coke and coal tar are sold outward, cutting long-distance raw-coal transport costs and improving overall mine profitability.
- Coal-chemical deep-processing enterprises: Serves as pre-treatment unit for coal deep processing to recover coal-tar in advance. Semi-coke is sent to subsequent gasification and combustion procedures to build a circular coal-chemical industrial chain.
- Municipal & industrial clean-fuel projects: Produces premium smokeless semi-coke as substitute for raw bulk coal for industrial boilers, civil heating and ore smelting, assisting local authorities in clean-energy transition.
- Coal-resource-oriented industrial parks: Acts as core pyrolysis unit inside coal-chemical parks, matching with tar distillation and carbon-material deep-processing enterprises. It shares park utilities and enjoys preferential park policies.
- Coal-technology R&D & demonstration bases: Used for coal-pyrolysis process research, adaptability tests for various coal types and new-technology demonstration. It supports multi-parameter experimental tests for coal samples.
Packing & Shipping
Packing Method:
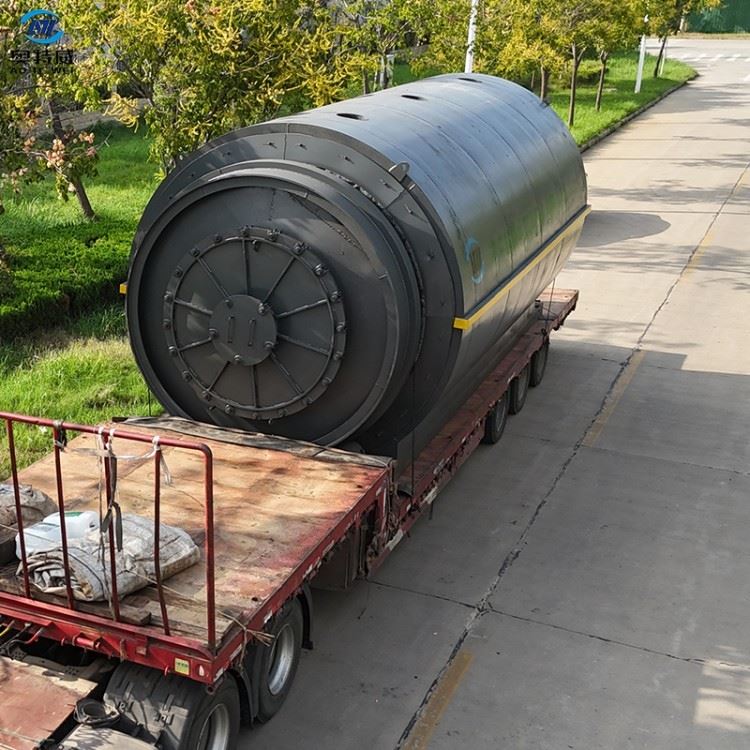
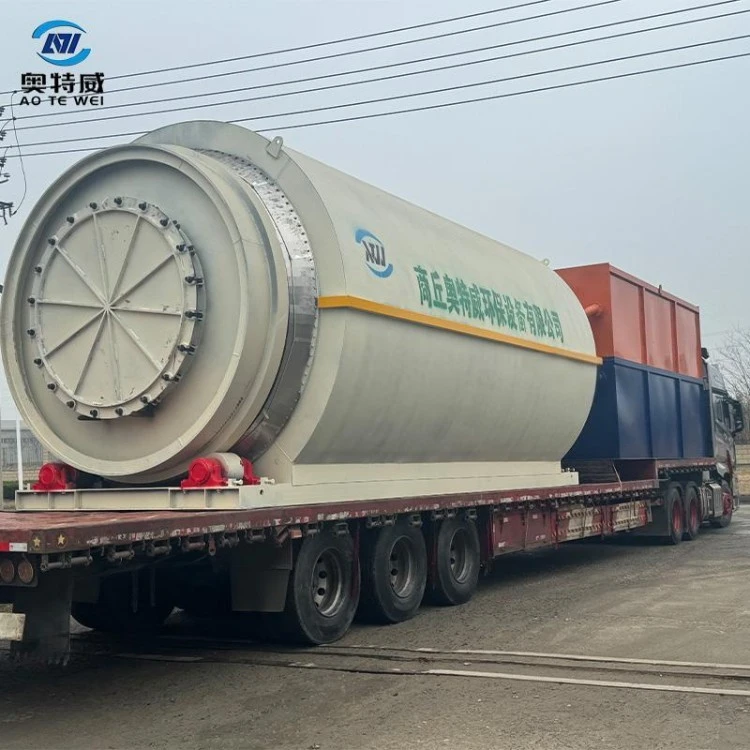
Reactor surface is coated with high-temperature anti-rust paint and wrapped with heavy-duty waterproof tarpaulin with pre-reserved lifting lugs. Gear rings, supporting rollers and wearing parts receive separate anti-collision protection. Electric-control cabinets, sensors and precision instruments are packed in shock-proof and moisture-proof plywood wooden crates. Pipes, gaskets, fasteners and spare parts are sorted and fixed on export pallets. English-language operation manuals, process-flow drawings, assembly drawings and detailed packing lists are supplied together.
Shipping Method:
Standard-capacity modules are split and loaded into multiple 40HQ containers for sea export. Extra-large reactor segments are shipped by break-bulk vessel. Heavy-duty flat-bed trucks deliver modules directly to site for inland transportation. All over-size components undergo centre-of-gravity calculation and reinforcement to avoid deformation and collision damage in transit
Delivery Lead Time:
85-110 working days upon advance-payment receipt for manufacturing, welding flaw-detection and factory no-load testing. Lead-time will be extended for orders with full-set auxiliaries or special custom requirements. Pre-shipment real-product photos, flaw-detection reports and factory test videos are provided for customer site preparation.
FAQ
Q1: What coal types are suitable? What is the regular processing capacity?
A: Mainly applicable to lignite, long flame coal, non caking bituminous coal and coal slime. Standard single batch throughput ranges from 6 10 tons. Highly caking coking coal is not suitable. A coal sample analysis report is required for accurate product yield prediction.
Q2: What products can be obtained from raw coal pyrolysis and what are the yield ratios?
A: Output varies with raw coal quality. Reference range: coal tar 6 12 %, semi coke 55 70 %, pyrolysis coal gas 12 20 %. Output proportions differ significantly among various coal types.
Q3: Does the equipment require non stop 24 hour running?
A: This is batch type equipment. Intermittent production is allowed according to raw coal supply and product sales conditions. Continuous non stop operation is not mandatory.
Q4: What site and foundation requirements are there for installation?
A: A 120 220 ㎡ hardened workshop area is required. Medium load concrete foundation is needed (higher load bearing requirement than plastic / tyre pyrolysis plants). Geological data shall be provided for foundation drawing design. Good ventilation and drainage systems are necessary for the site.
Q5: Can coal crushing screening and semi coke cooling systems be added at a later stage?
A: Yes. The equipment reserves interfaces for front end coal pre treatment and back end semi coke post processing modules. Auxiliaries can be added without modifying the main reactor body.
Q6: What are the warranty terms?
A: 1 year whole set warranty for non human caused damage; 3 year warranty for main reactor body. Consumable wearing parts are supplied at cost price on a long term basis.
Product Certification
Our coal pyrolysis equipment series has passed multiple inspections and certifications complying with international standards:
- Pressure-vessel manufacturing compliance: All reactor shells are manufactured in accordance with domestic pressure-vessel standards. Welding non-destructive testing and pressure-resistance tests are completed before delivery. Complete manufacturing-inspection reports are available.
- CE compliance: Core electrical, control and transmission components satisfy CE standards to support market access for Europe and global destinations.
- Third-party pre-shipment inspection: Authorized third-party institutions such as SGS and BV can perform witness inspection, dimension verification and functional testing upon customer request.
- Environmental-protection-test reports: Flue-gas-emulation test reports are provided as reference documents for customers' local environmental-protection-approval applications.
- Complete documentation package: Manufacturing records, material certificates for steel plates and key components and various test reports are supplied, supporting customers for import customs clearance and project filing procedures.
Hot Tags: coal pyrolysis plant, China coal pyrolysis plant manufacturers, suppliers, factory


